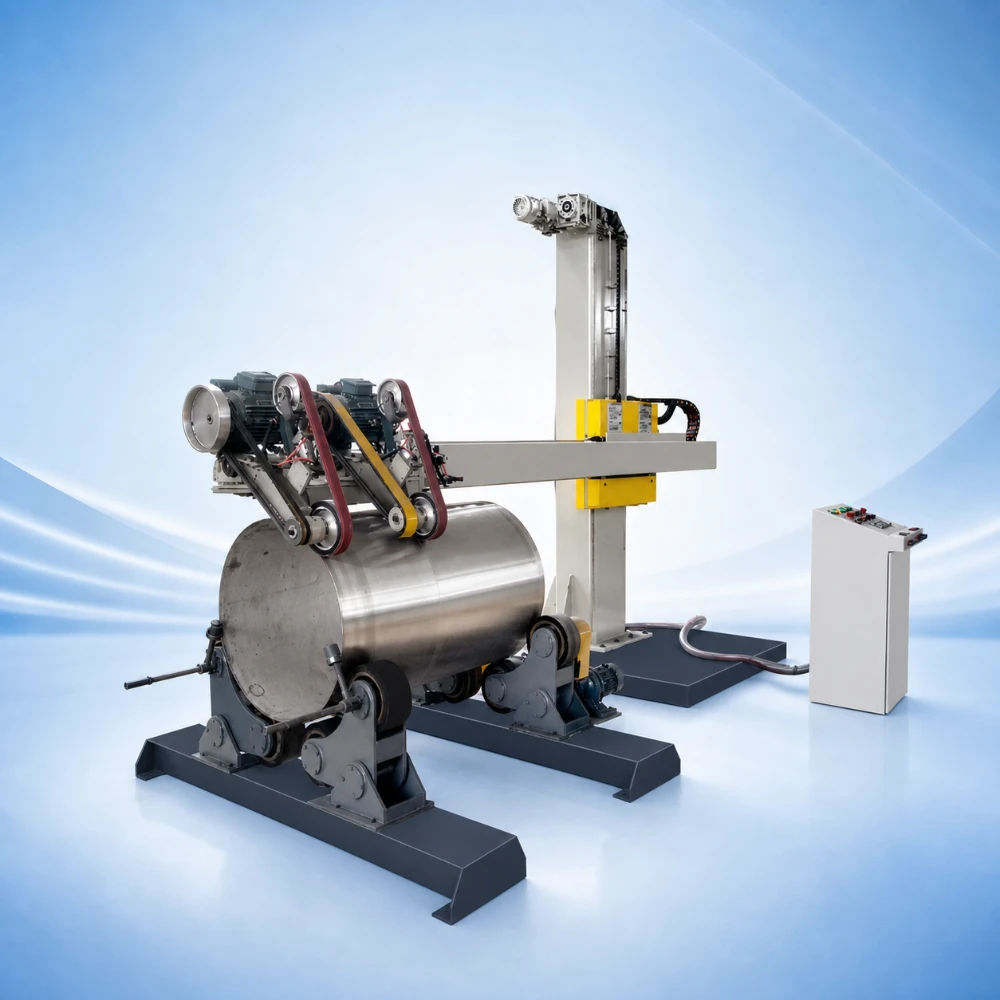
Cookware Polishing Matched to the Formed Body
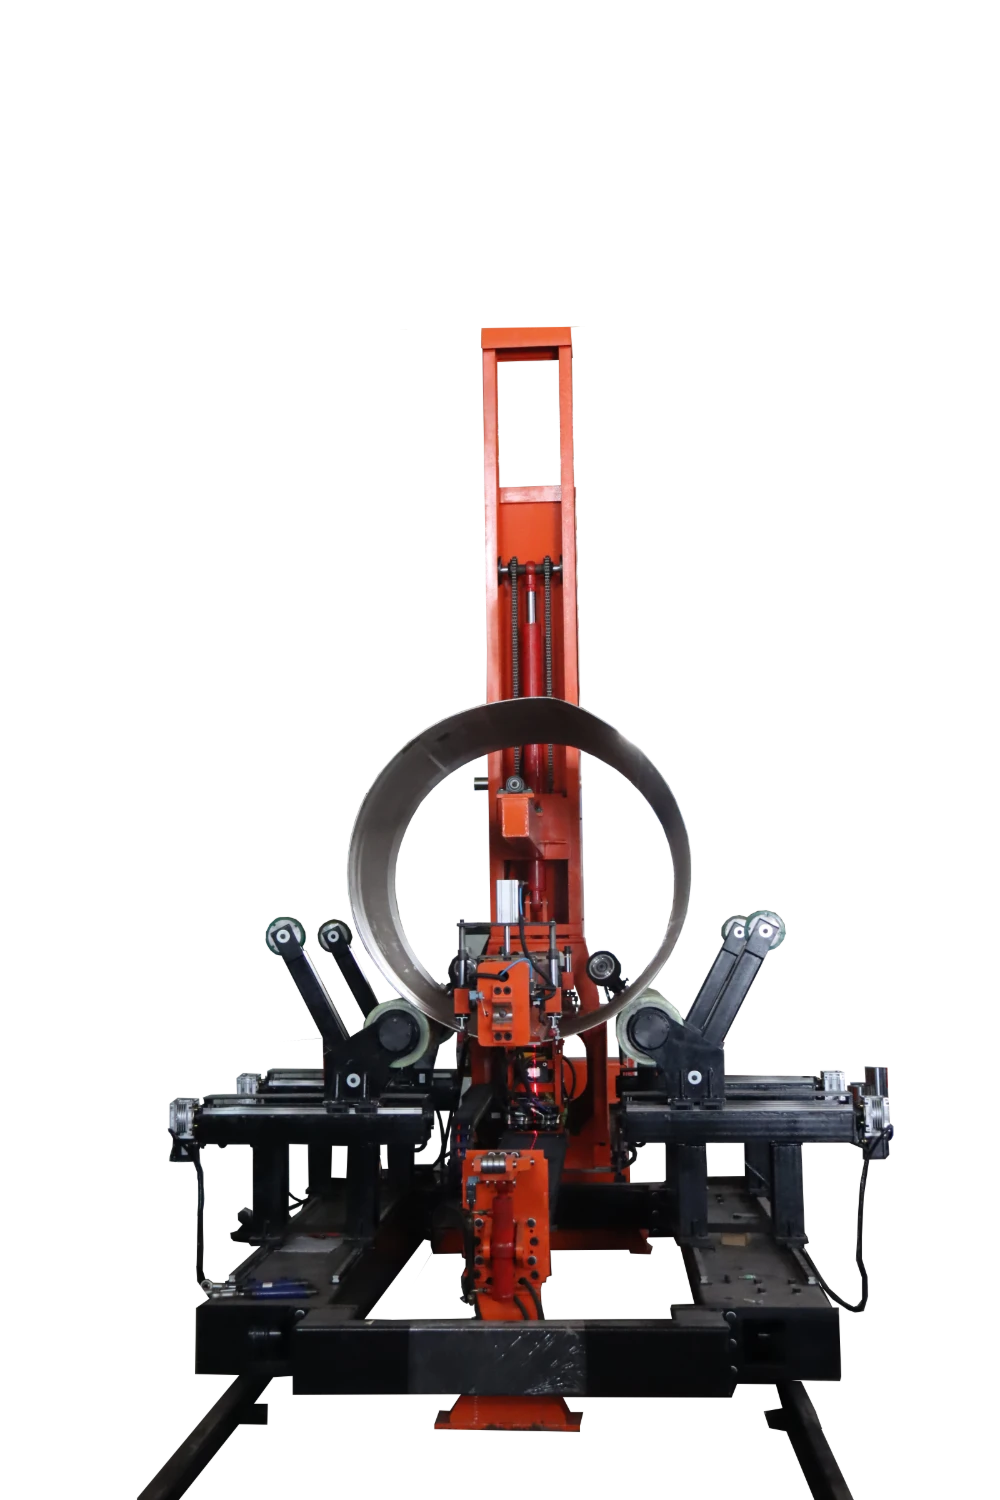
This cookware polishing application is for manufacturers of stainless-steel and aluminum pots, pans, kettle bodies and pressure-cooker bodies that need an agreed surface appearance on formed metal components. Equipment, fixtures and abrasives are selected around the actual cookware profile, processing area and production stage rather than a single assumed standard machine.
The first selection question is where the tool must work: interior wall, exterior wall, base, rim or the wall-to-base transition. A deep pot and a shallow pan can need different holding and contact arrangements even when their diameters are similar.
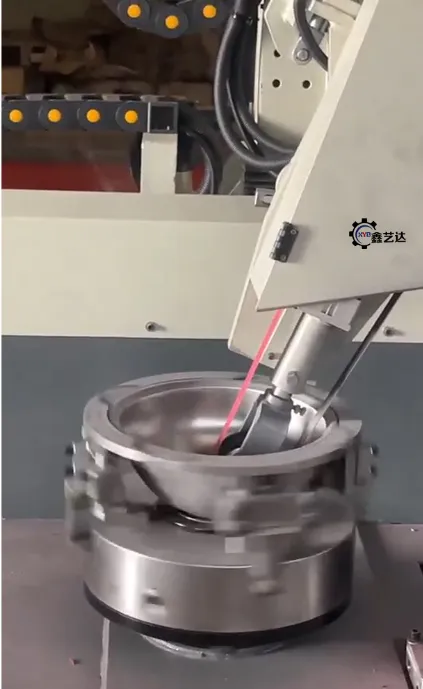
Define the Finishing Regions
- Interior wall and base: show vessel depth, opening and corner radius, including regions the tool must reach.
- Exterior body: review the profile, formed features and attachment points that affect contact or holding.
- Rim and transitions: identify the edge shape that must be retained and any areas excluded from polishing.
- Assembled or coated parts: identify handles, fittings, coatings and the production stage before choosing a process.
These are separate application requirements. They do not mean one standard fixture finishes every surface in a single cycle. Thin walls also require a review of support, contact and the permitted material-removal allowance.
Agree the Starting Surface and the Target Appearance
Forming marks, prior grinding and scratches determine how much preparation is needed. A brighter or mirror-like finish depends on the material and abrasive sequence; a deep mark cannot be assumed removable within every wall-thickness allowance. Use a reference sample and define permitted marks before comparing a production trial.
Workpiece Information for Configuration
| Selection detail | Information required |
| Product geometry | Drawing, diameter, depth, profile and opening size. |
| Material | Alloy, construction and wall thickness. |
| Processing area | Inside, outside, bottom or a defined combination. |
| Incoming surface | Forming marks, scratches and previous preparation. |
| Required result | Reference sample, permitted defects and dimensional allowance. |
| Production | Batch sizes, product changeovers and target cycle time. |
Review Handling Features and Protected Surfaces
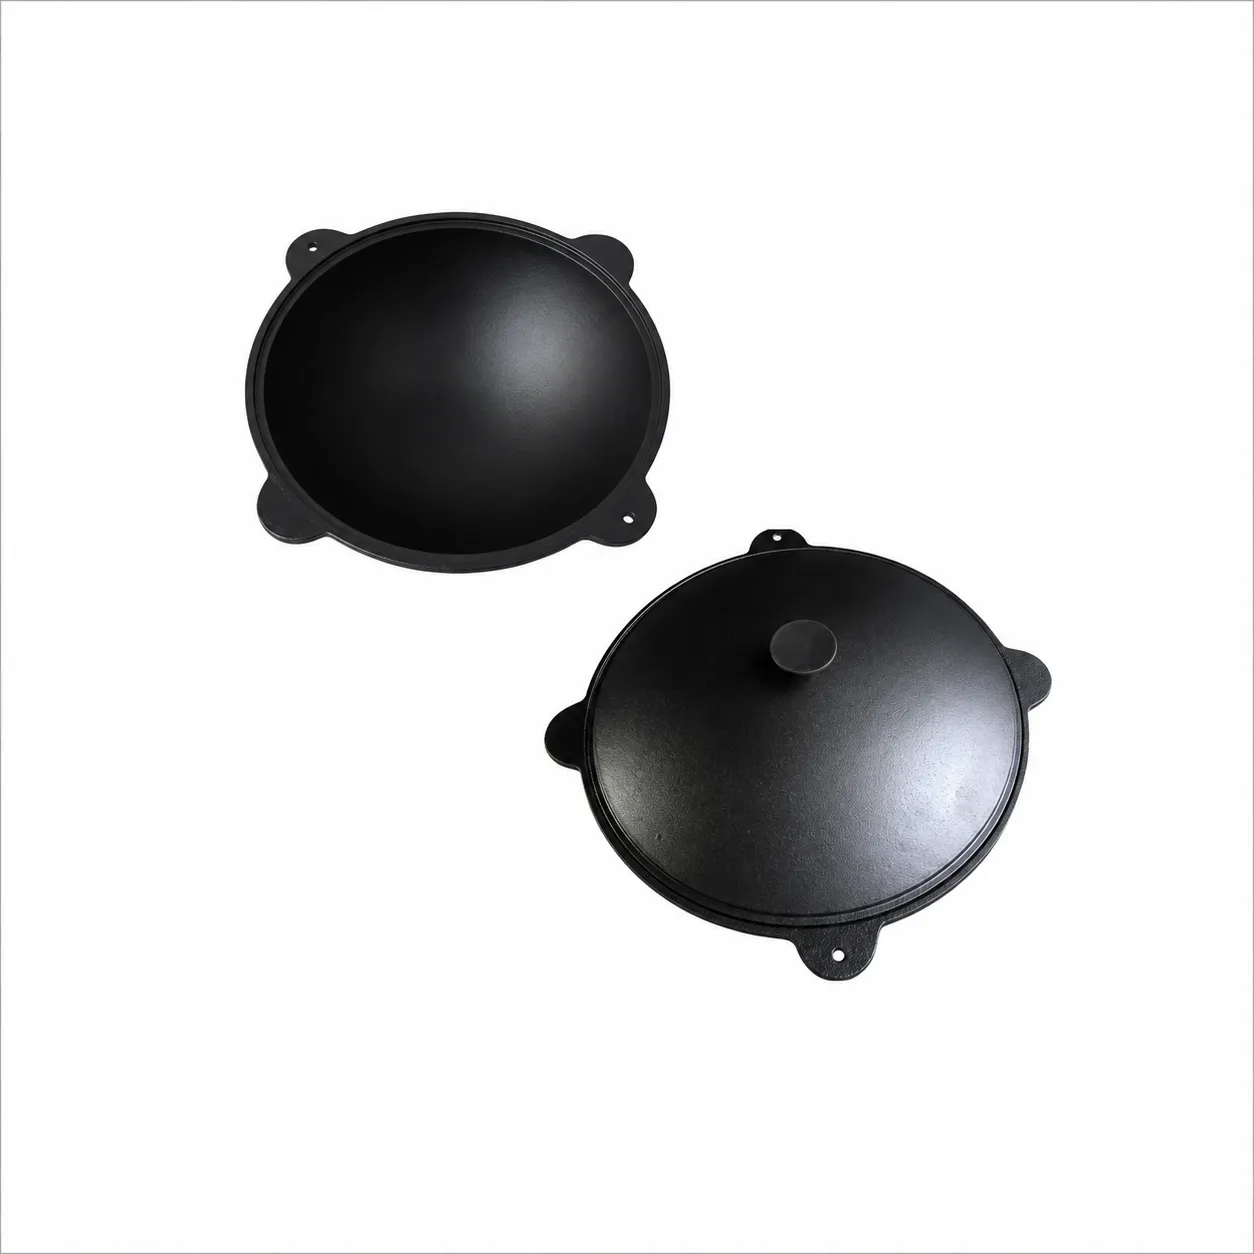
Rims, handles and coatings can restrict tool access or require a different processing stage. Mark every protected area on the part drawing and clarify whether polishing occurs before or after attachment or coating. Do not assume an assembled product can be processed without removing or protecting features.
Approve the Part Before Scaling Production
- Supply the formed part, material grade, wall thickness and initial surface.
- Review the fixture, tool entry and all required finishing regions.
- Develop preparation and polishing stages for the approved appearance and removal allowance.
- After cleaning, check the interior and exterior appearance, retained profile, handling marks and dimensional change.
- Measure loading, processing, tool/fixture changes and inspection for each cookware size.
This page does not publish a confirmed fixed model, motor power, workpiece capacity or cycle time. Those details need a matched equipment specification and representative cookware trial. Polishing alone does not establish food-contact compliance or pressure integrity.
A flat part such as a separate metal base requires its own holding and surface review; compare the Flat Metal Mirror Polishing Machine only where that workpiece geometry is applicable. Other shape-specific configurations are listed under customized machines.