Straight-Seam Welding for Cabinets, Enclosures and Metal Boxes
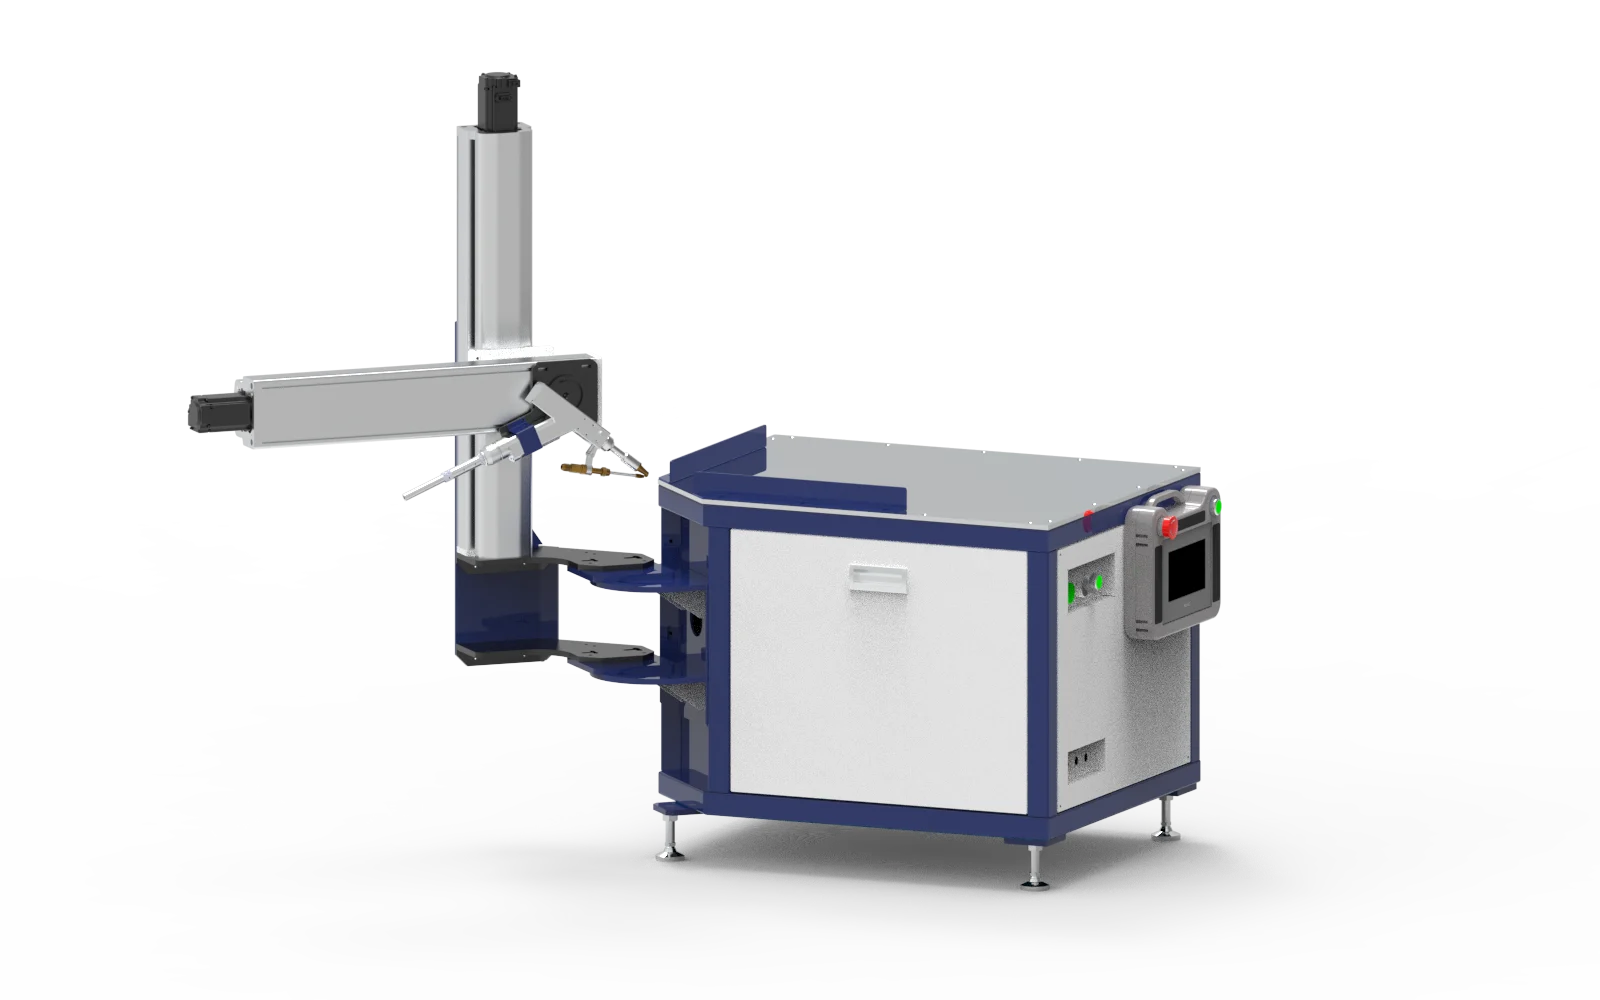
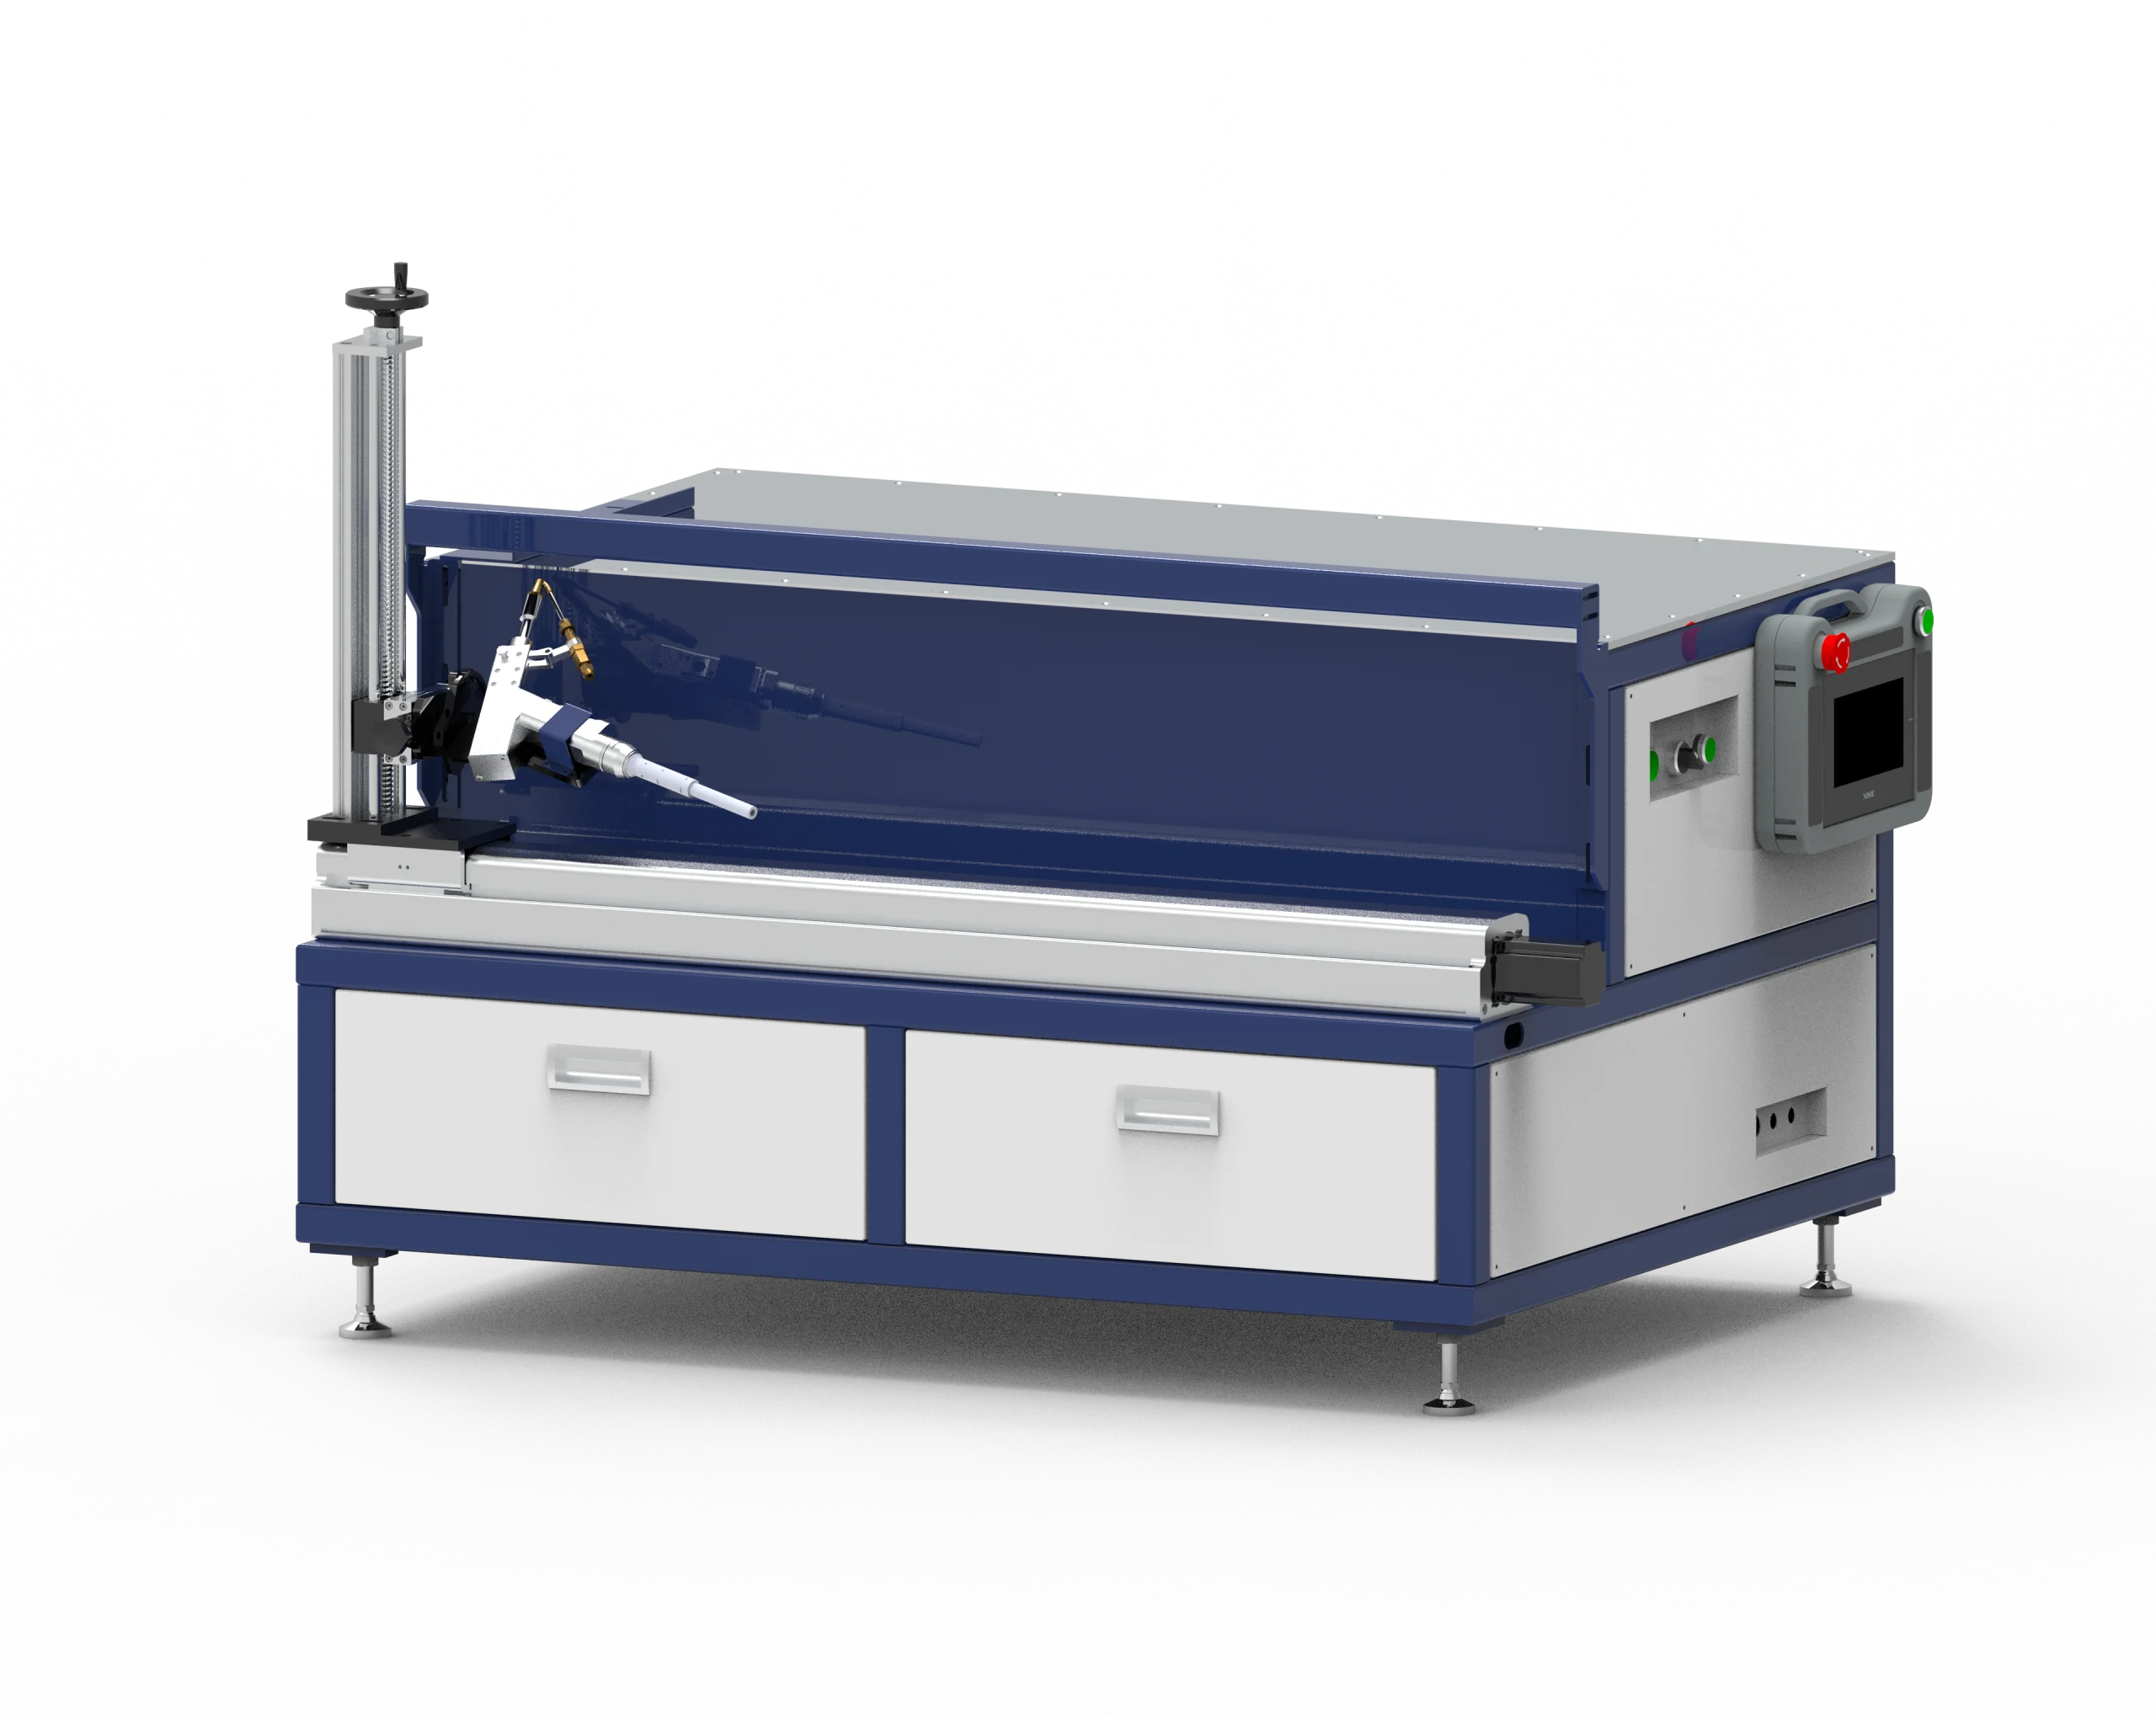
The Horizontal Straight Seam Welding Platform is for fabricators producing repeated straight outer-corner joints on sheet-metal assemblies. A servo-driven carriage and PLC-controlled path support consistent torch movement while the workpiece is held in a defined fixture.
It is particularly relevant when operators repeat the same accessible seam on cabinets, equipment housings, battery boxes or kitchen-equipment components. Assess the part orientation, clamping method and complete joint access before selecting a travel length.
Workholding Comes Before Automation
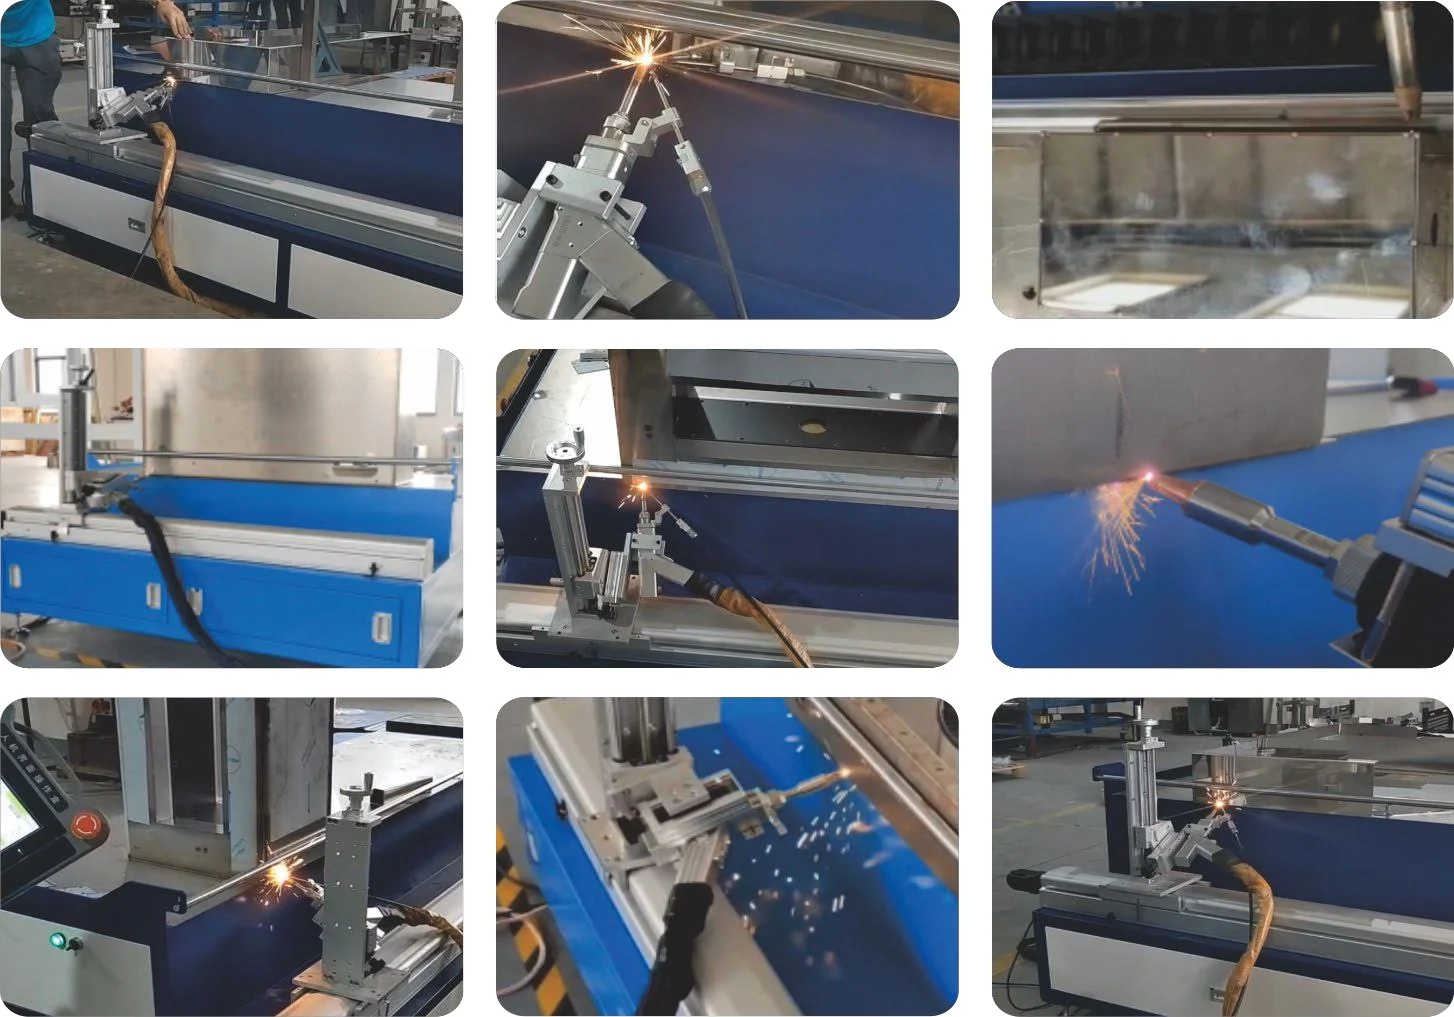
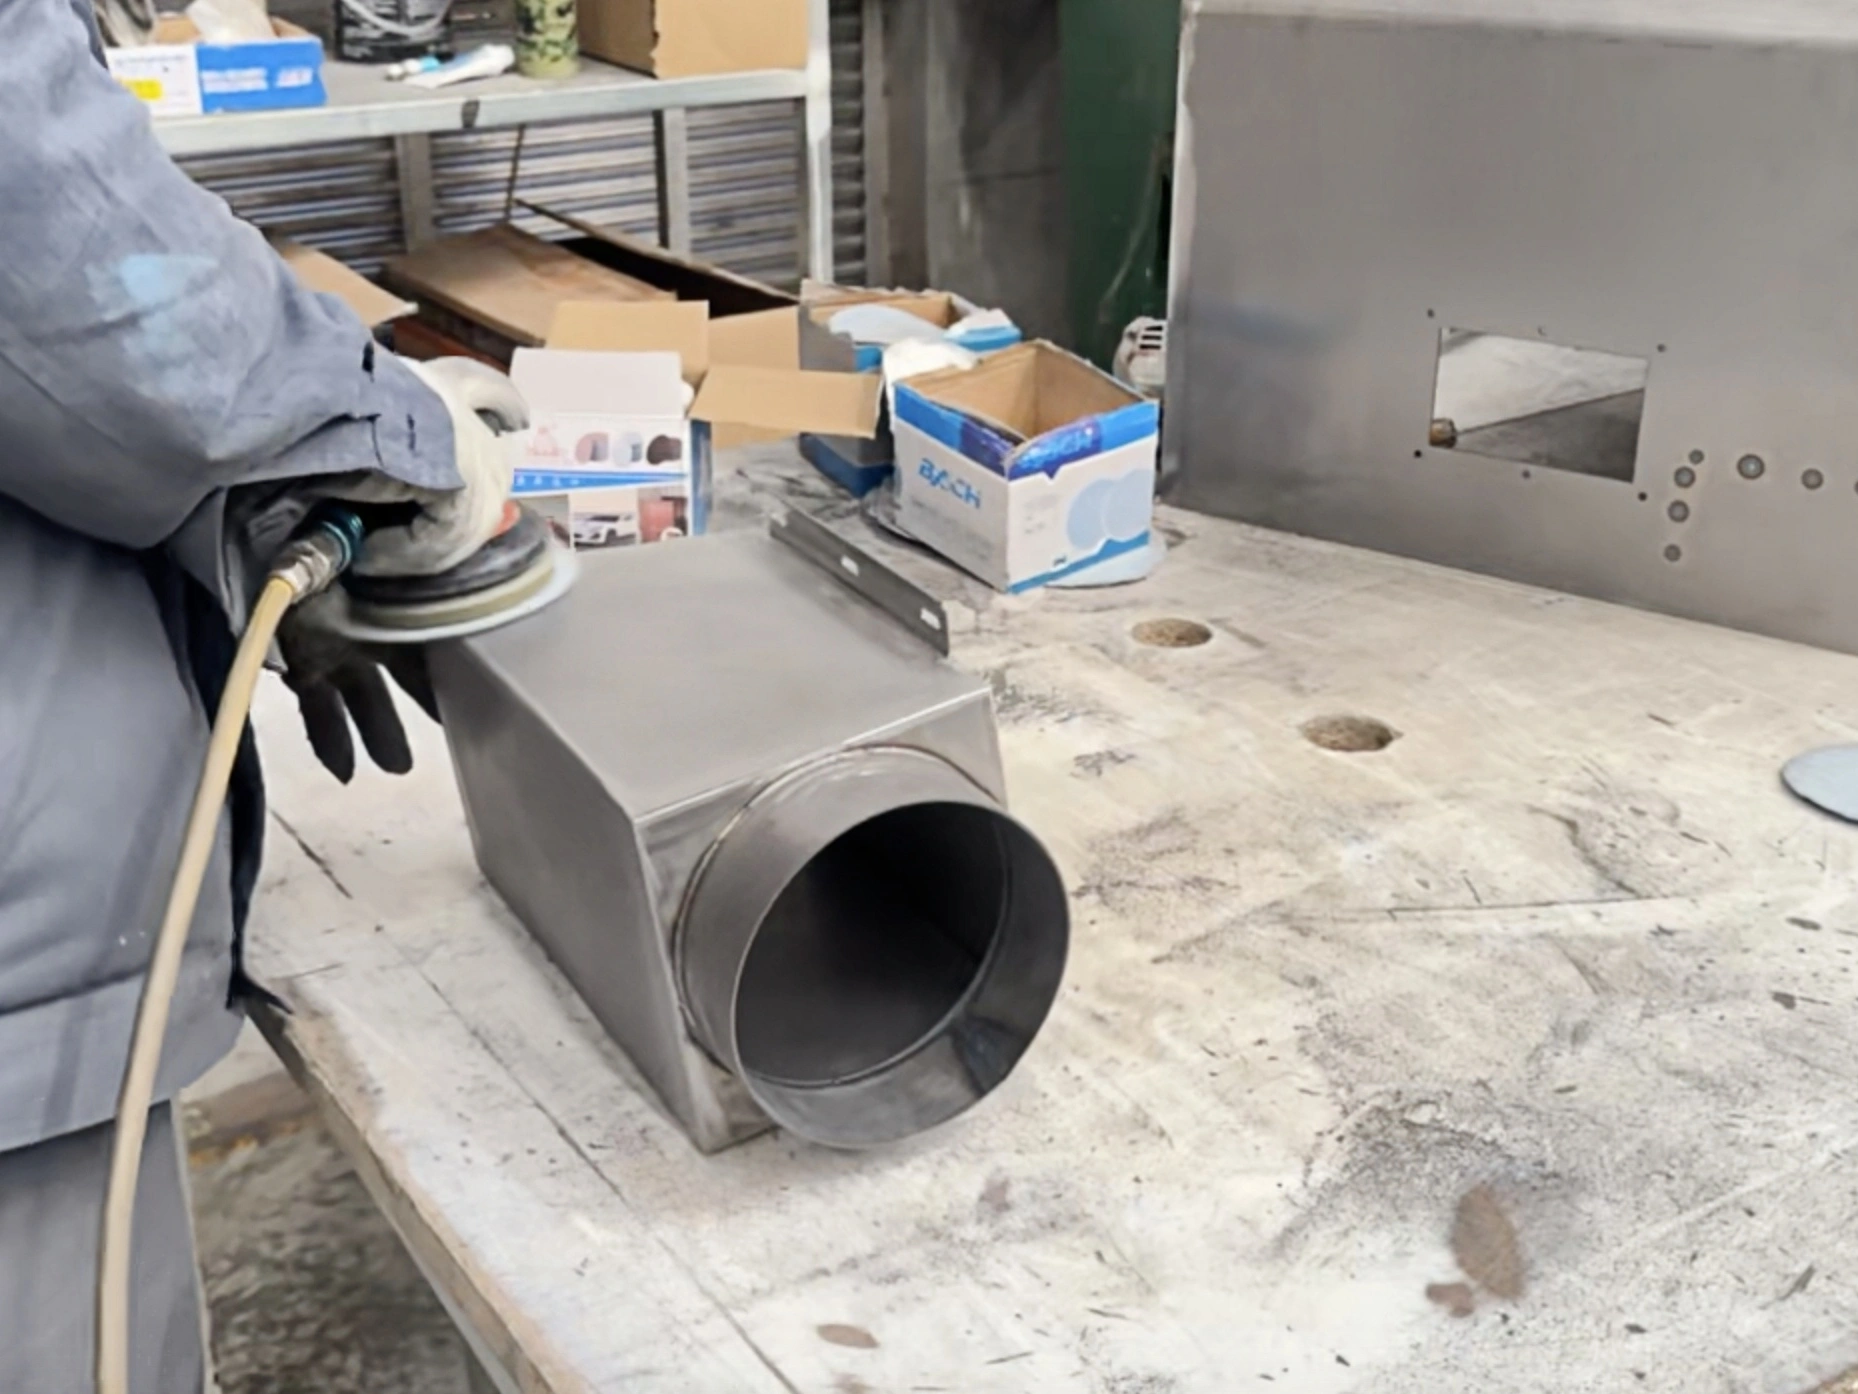
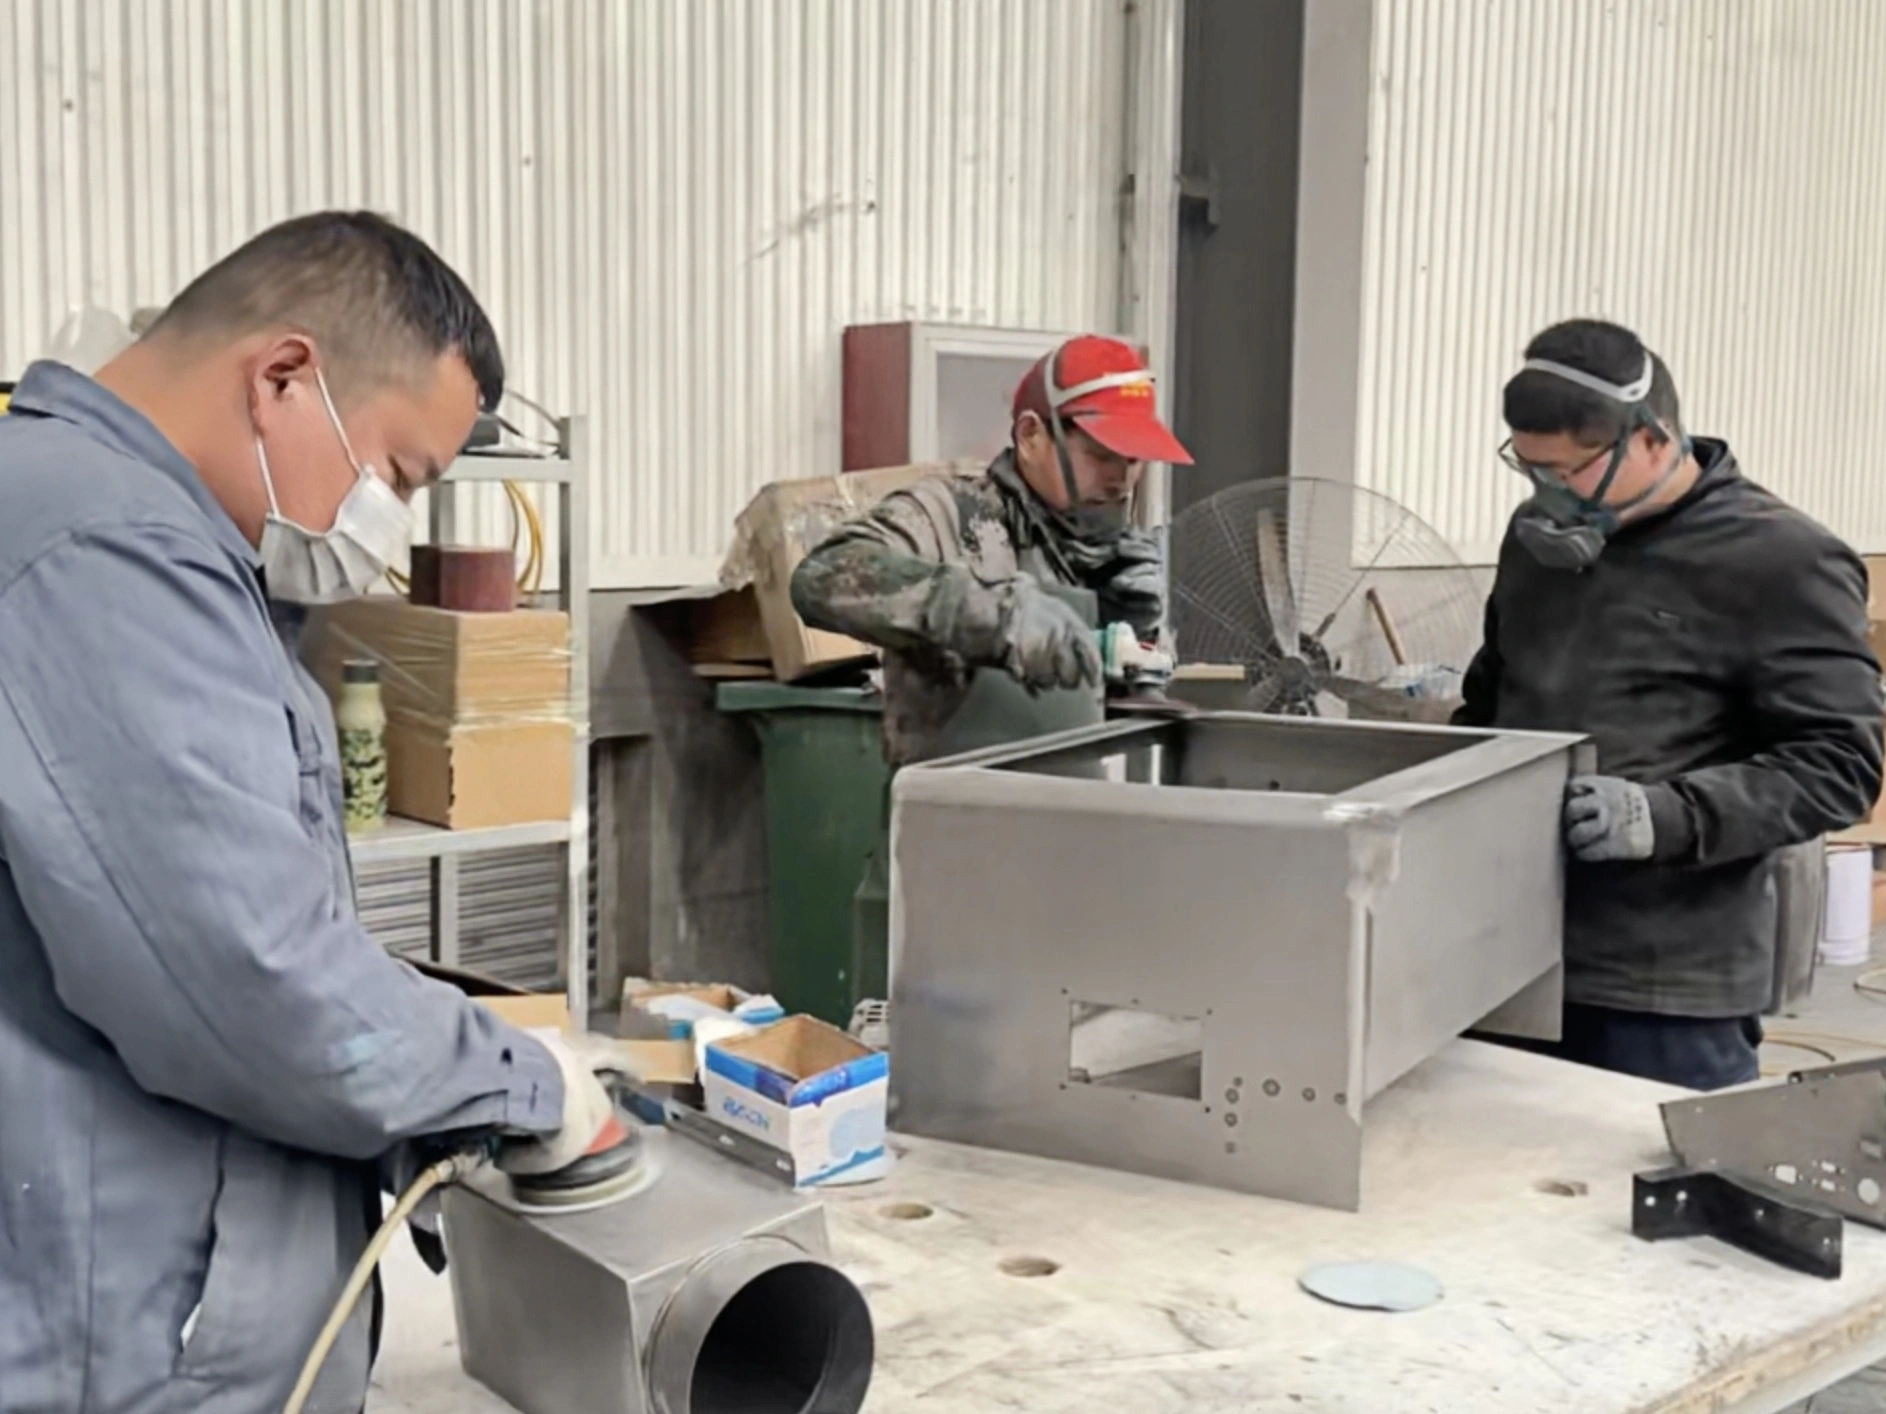
The application photographs illustrate head access and support arrangements, not a universal fixture. The selected tooling must hold the joint without blocking the start, end or any programmed segment. Include flanges, folds and adjoining panels in the drawing used for the fixture review.
- Joint consistency: define locating points, fit-up and the acceptable gap for the selected welding process.
- Head clearance: allow room for the torch or laser head, filler-wire access and cables.
- Loading sequence: evaluate clamping, welding and unloading as one workstation cycle.
Program the Required Seam Pattern
Touchscreen settings, manual/automatic modes and foot-operated start support setup and repeated cycles. Continuous, spot, stitch and multi-segment modes allow the travel sequence to follow the joint drawing. A programmed path does not compensate for inconsistent fit-up or an unsuitable welding source.
Approve the Weld on Your Material
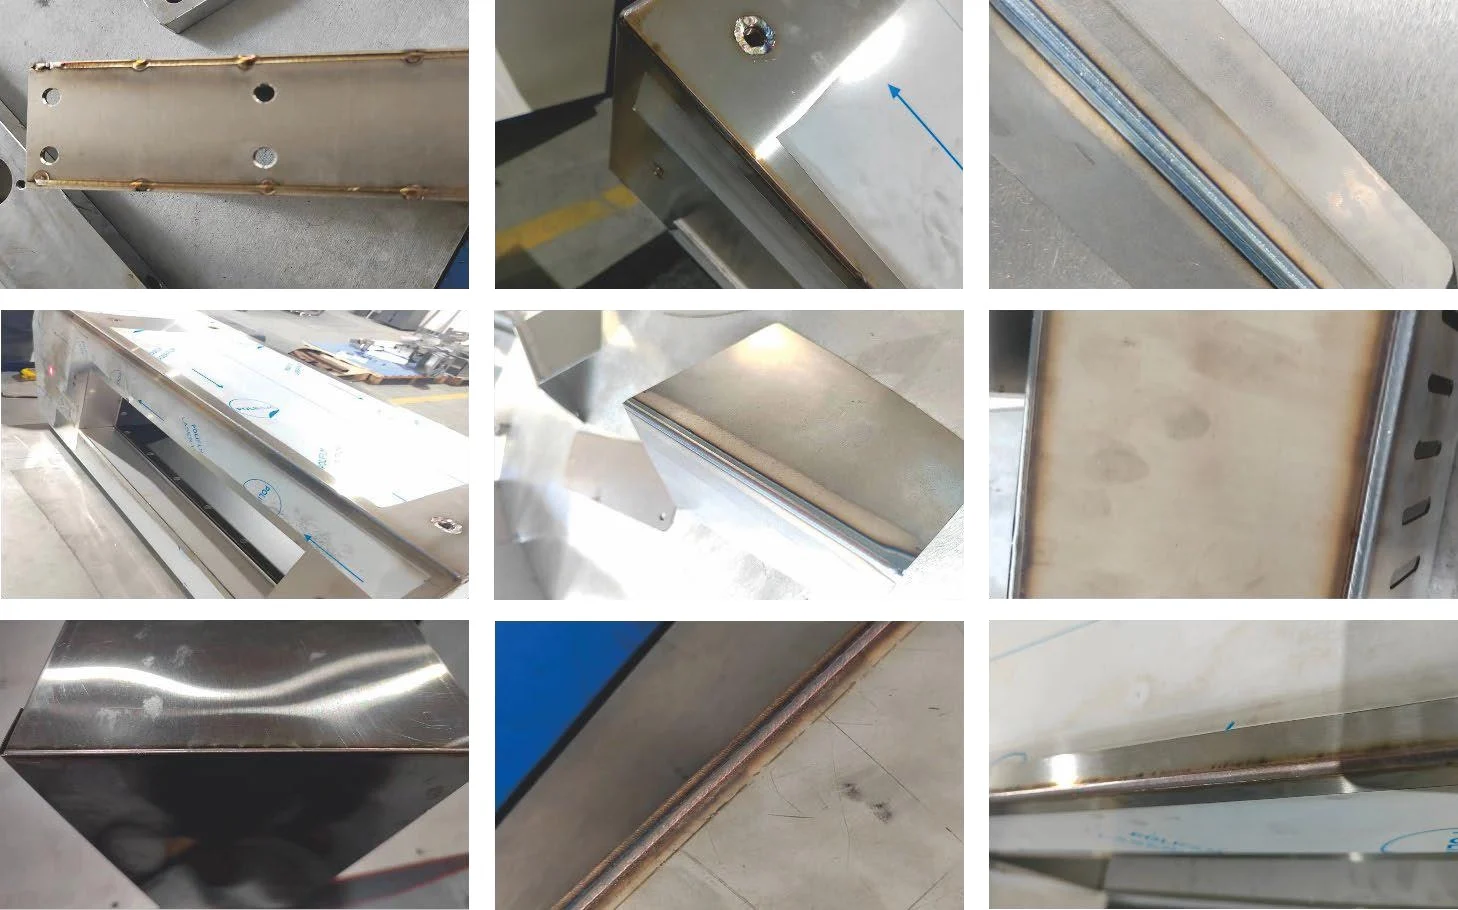
These weld samples are application references. Agree the required penetration, visible bead, acceptable discoloration and inspection method on your own material and joint. Do not infer structural weld acceptance or identical appearance from photographs alone.
The listed material applications are stainless steel, carbon steel and aluminum alloy, with a published 0.4-6 mm plate-thickness range. The actual workable thickness depends on source power, material, joint preparation and process settings.
Published Model Comparison
| Parameter | BR-HJPT-1000mm | BR-HJPT-1600mm | BR-HJPT-2000mm |
|---|---|---|---|
| Y-axis effective travel | 1000 mm | 1600 mm | 2000m in source; unit to confirm |
| Travel drive | Servo | Servo | Servo |
| Control system | PLC | PLC | PLC |
| Equipment dimensions (source values) | 1250 x 940 x 640 | 1850 x 990 x 640 | 2250 x 990 x 640 |
| Weight | 165 kg | 220 kg | 350 kg |
| Power supply | Single-phase AC 220 V +/-10%, 50 Hz | Single-phase AC 220 V +/-10%, 50 Hz | Single-phase AC 220 V +/-10%, 50 Hz |
Capacity clarification: the original 2000-model travel is printed as "2000m" and the equipment dimensions omit a unit. Confirm both entries for the named model. Motion travel is not necessarily effective welding length: the approved path and fixture clearance must leave room at both ends. The table retains the current product-page values.
Integrate the Welding Source
Laser, TIG and gas-shielded sources are listed options, subject to torch mounting and the source-control interface. Review cooling, shielding gas and filler requirements with the chosen process. The stated electrical supply is for the platform; check the source and auxiliary equipment separately.
Define which items are supplied: platform, welding source, torch holder, fixtures, cooler, wire feeder and safety equipment. Welding consumes process-specific materials even when the positioning platform itself uses no abrasive consumables.
Prepare a Part-Based Acceptance Trial
- Provide a dimensioned drawing, material grade, thickness and representative incoming parts.
- Specify straight seam length, joint orientation, required welded/unwelded sections and fixture locations.
- Identify the existing welding source and the required head/control connections.
- Agree penetration, appearance and inspection criteria; measure the complete loading-to-unloading cycle.
Compare the Vertical Corner Welding Platform when upright outer-corner joints suit the loading arrangement better. The Horizontal Automatic Welding Platform also lists a horizontal travel configuration; confirm the exact model and scope rather than assuming the pages describe interchangeable equipment.
English Product Overview
A two-page overview covering application photographs, weld samples, process options and the information needed for configuration review. Published by ANHUI BONRAY CO., LTD. This overview is not an operating manual.