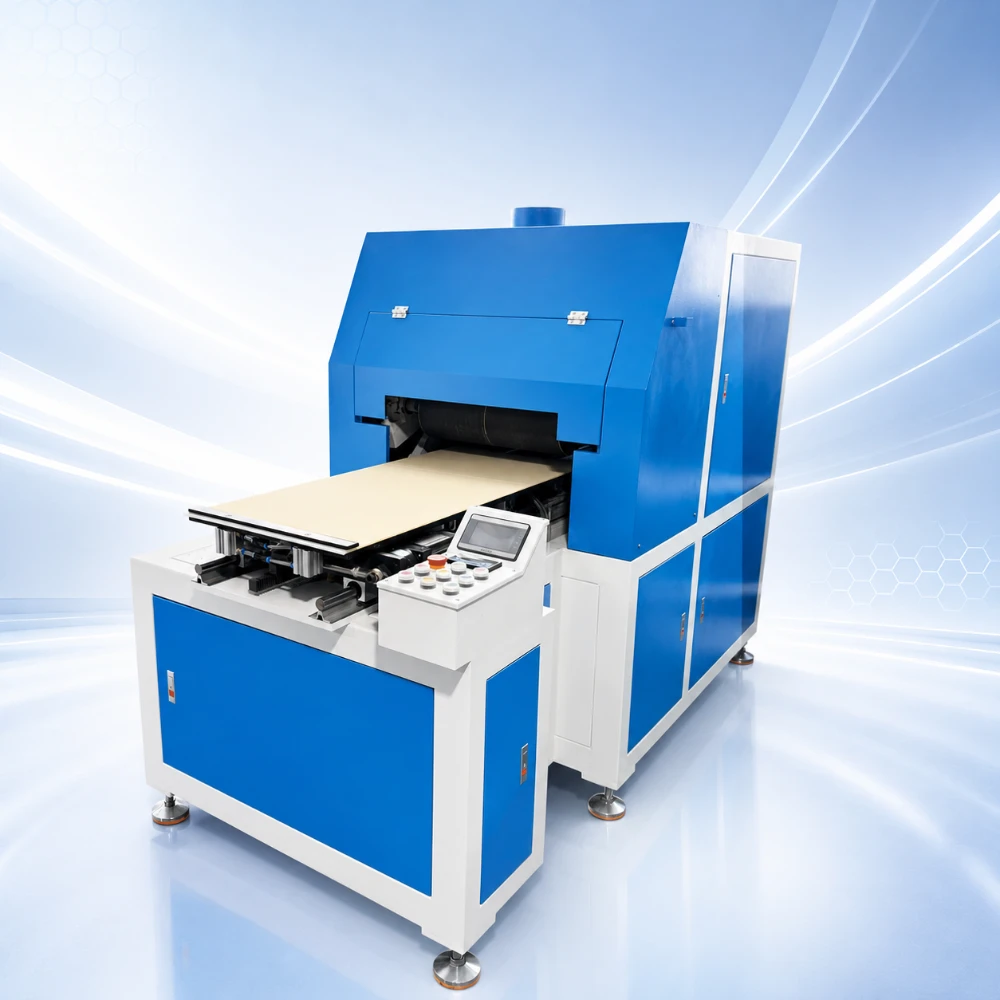
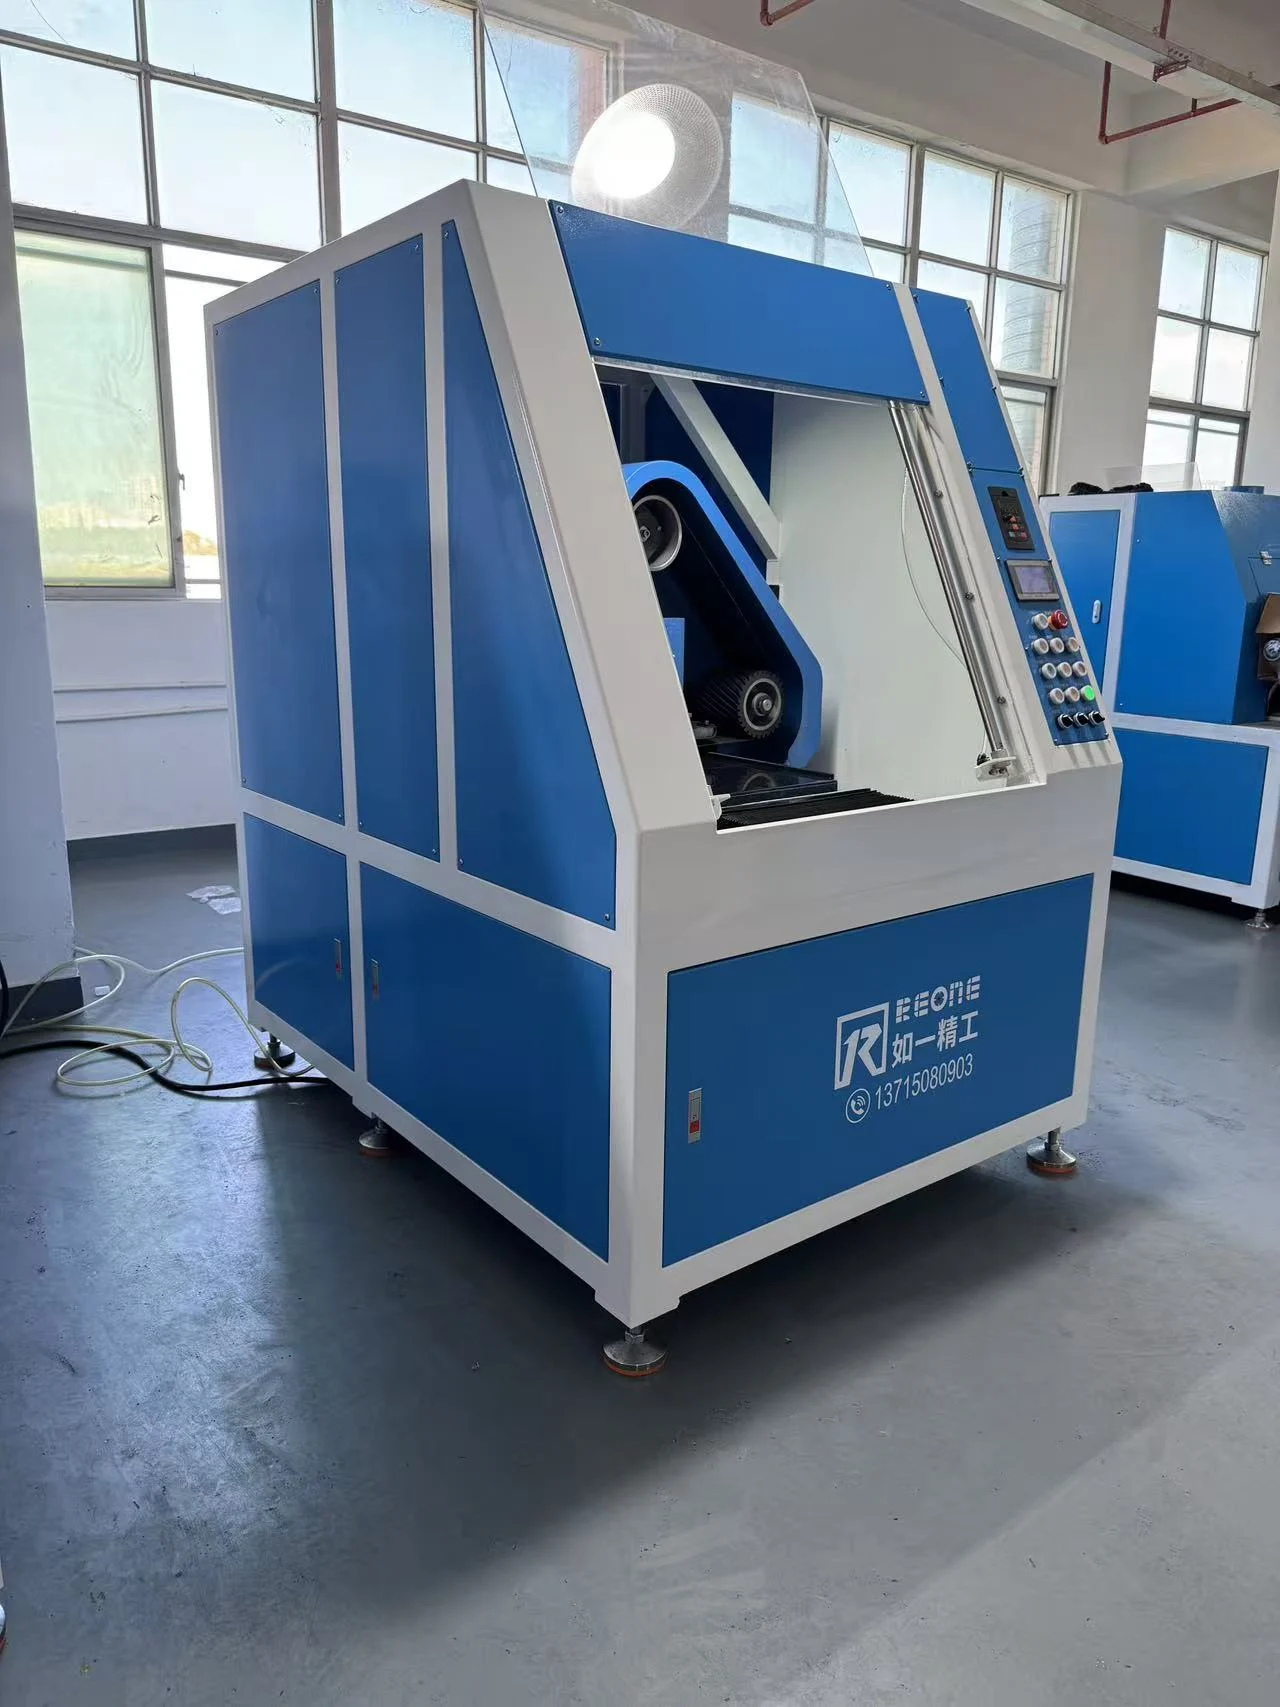
Wet Surface Polishing for Small Flat Metal Parts
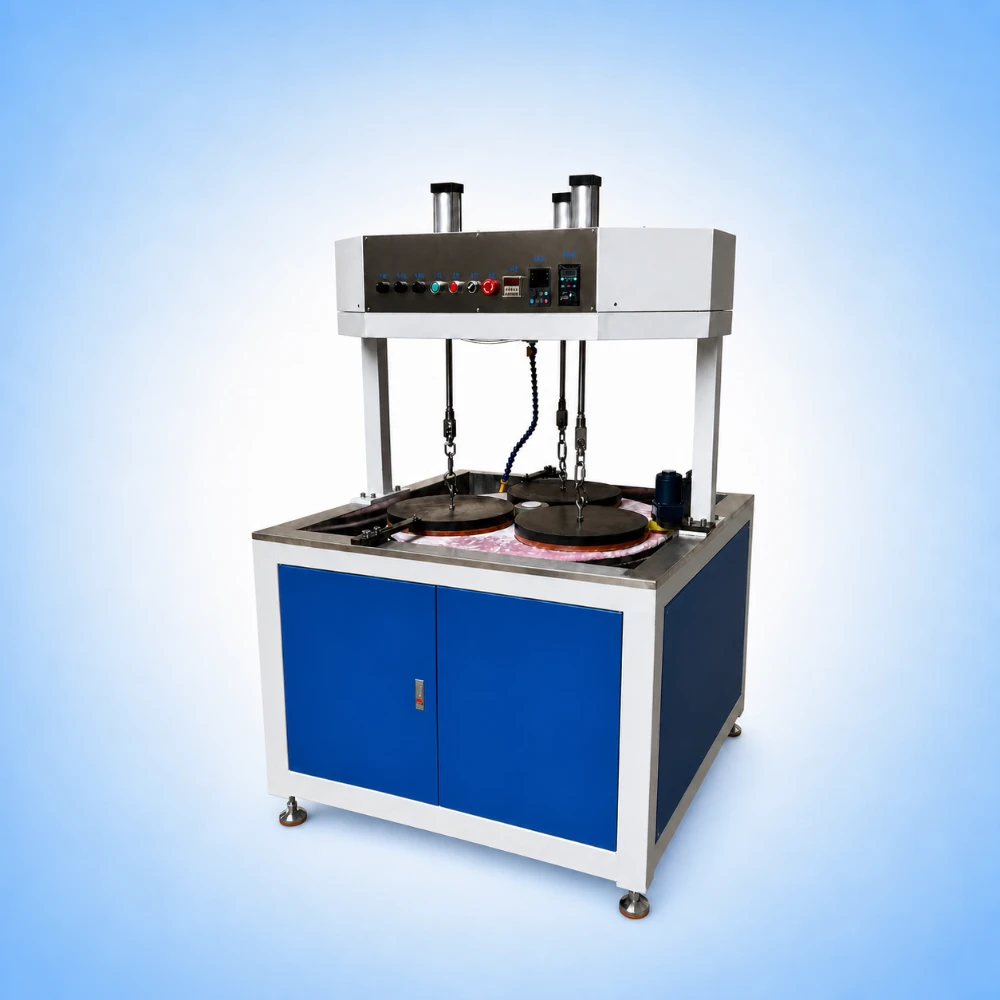
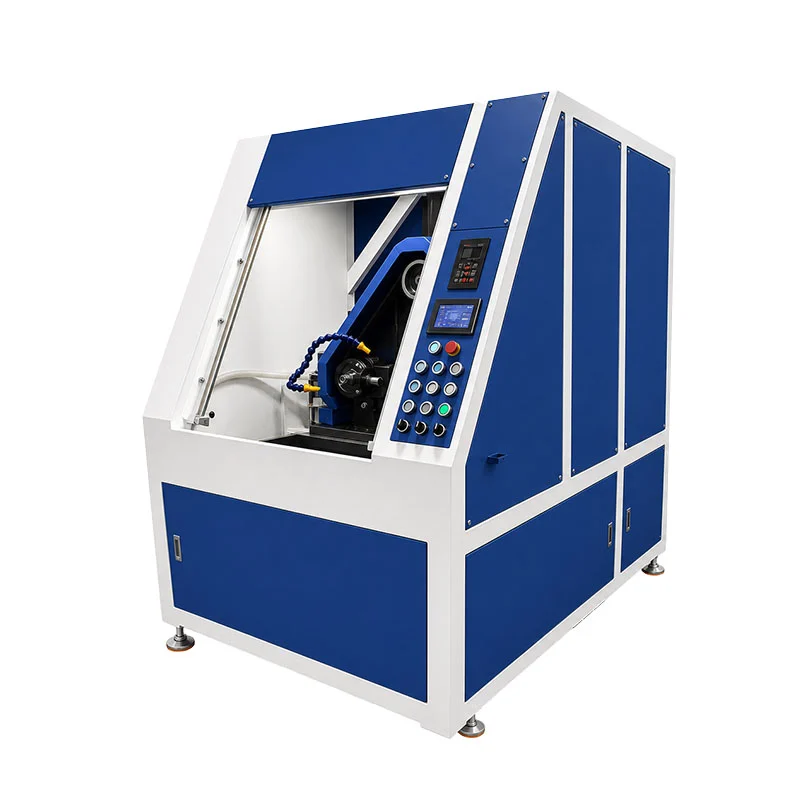
The BY-5030 Wet Metal Polishing Machine is for hardware manufacturers and finishing workshops refining accessible flat faces on small metal components. It is an application to assess when the workpiece, abrasives and cleaning method are suitable for a wet finishing process.
Start with the incoming surface and the delivered-part requirement: which marks must be reduced, which faces must remain untouched, and how the part will be held, cleaned and inspected. The machine name alone does not establish workpiece fit, wet-circuit scope or a guaranteed finish.
Match the Part to the Working Arrangement
- Hardware and fabricated components: exposed flat faces requiring a more consistent appearance.
- Suitable laser-cut parts: face finishing after cutting, with edge condition and protected features reviewed separately.
- Finishing subcontractors: repeat batches whose material, incoming surface and agreed finish can be assessed together.
Check length, width, thickness, flatness and clamping access. Overall dimensions do not specify the maximum part envelope. Deep pockets and inaccessible contours are not automatically reached by a flat-face polishing setup.
Plan the Wet Process and Cleanup
Confirm the actual supplied liquid-delivery and collection arrangement before planning installation. A pump, recirculation tank, filter or separator should not be assumed included. Select approved abrasives, polishing media and liquid for the installed tool arrangement and workpiece material.
- Preparation: identify scratches or fabrication marks and the amount of material removal permitted.
- Refinement: establish the compatible abrasive sequence and inspect between stages.
- Cleaning: review residue removal, drying and checks for staining, corrosion or contamination.
- Cycle planning: include loading, any repositioning, polishing, cleaning and inspection.
BY-5030 Published Specifications
| Parameter | Specification |
|---|---|
| Main motor | 3 kW x 1 |
| Feed motor | 0.55 kW x 1 |
| Swing motor | 0.25 kW x 1 |
| Voltage / frequency | 380 V / 50 Hz, or customized |
| Spindle speed | 1,430 r/min |
| Feed speed | 3.5 m/min; frequency-controlled |
| Swing frequency | 72 times/min; frequency-controlled |
| Worktable height | 750 mm |
| Listed achievable roughness | ≤0.2 µm after repeated polishing |
| Listed polishing time | 0-3 minutes per piece; application-dependent |
| Machine dimensions (L x W x H) | 1,300 x 800 x 1,350 mm |
Performance conditions: the listed roughness of ≤0.2 µm requires repeated polishing. The 0-3 minute/piece entry is application-dependent, not a zero-time cycle or guaranteed throughput. Agree the actual finish measurement, passes and complete-cycle time on a representative part.
Prepare a Wet-Process Trial
- Material grade and parts in their actual incoming surface condition.
- Dimensions, flatness, holding points, edges and features to protect.
- Approved appearance or roughness requirement and the inspection method.
- Allowed cleaning/drying method, batch target and available process utilities.
For a related flat-part buffing application, compare the Flat Metal Mirror Polishing Machine. For a reflective visual target, review the 8K Mirror Polishing Machine; neither page proves the same wet-process configuration.