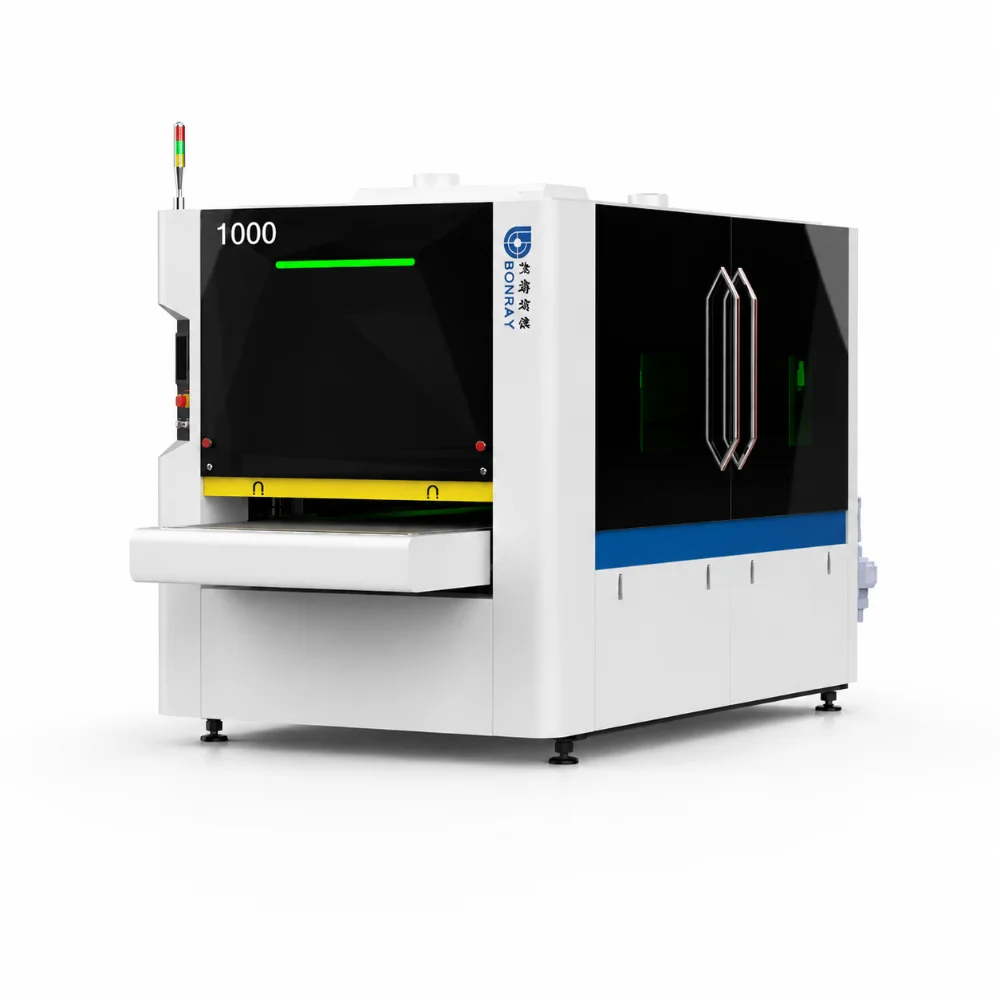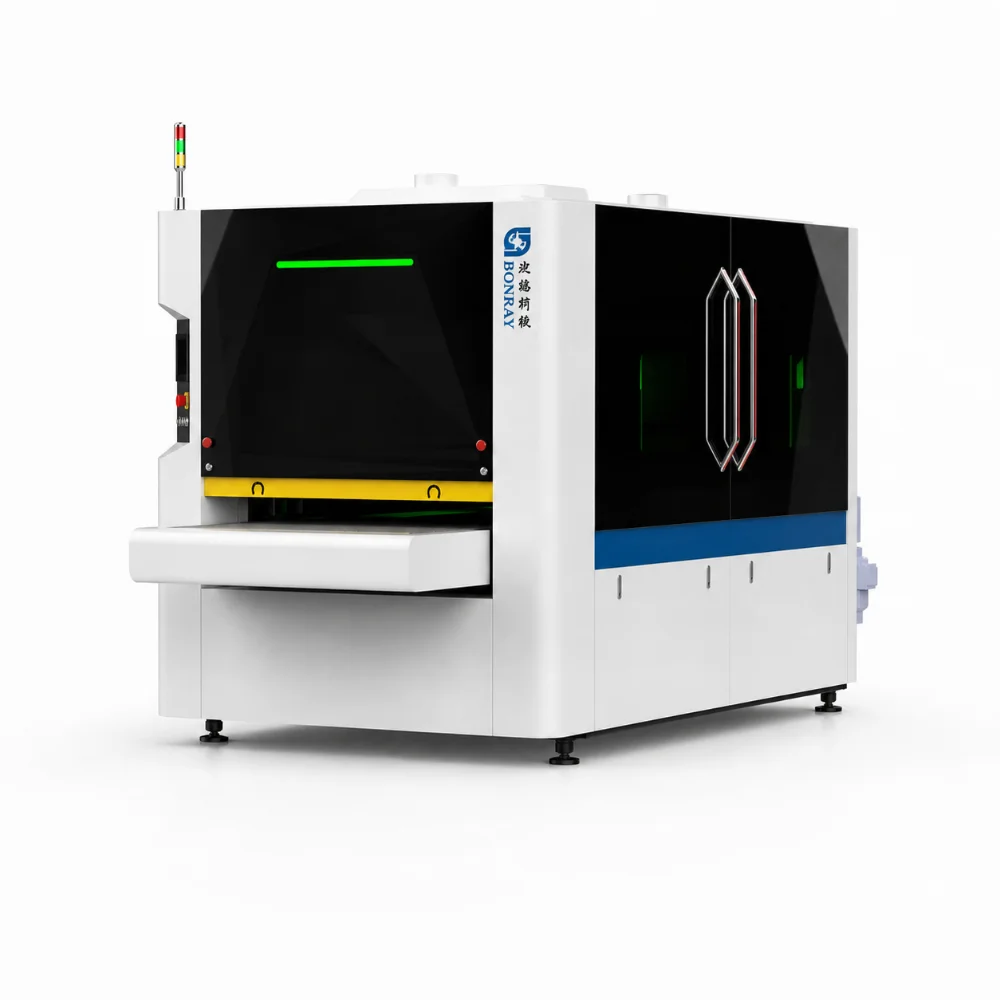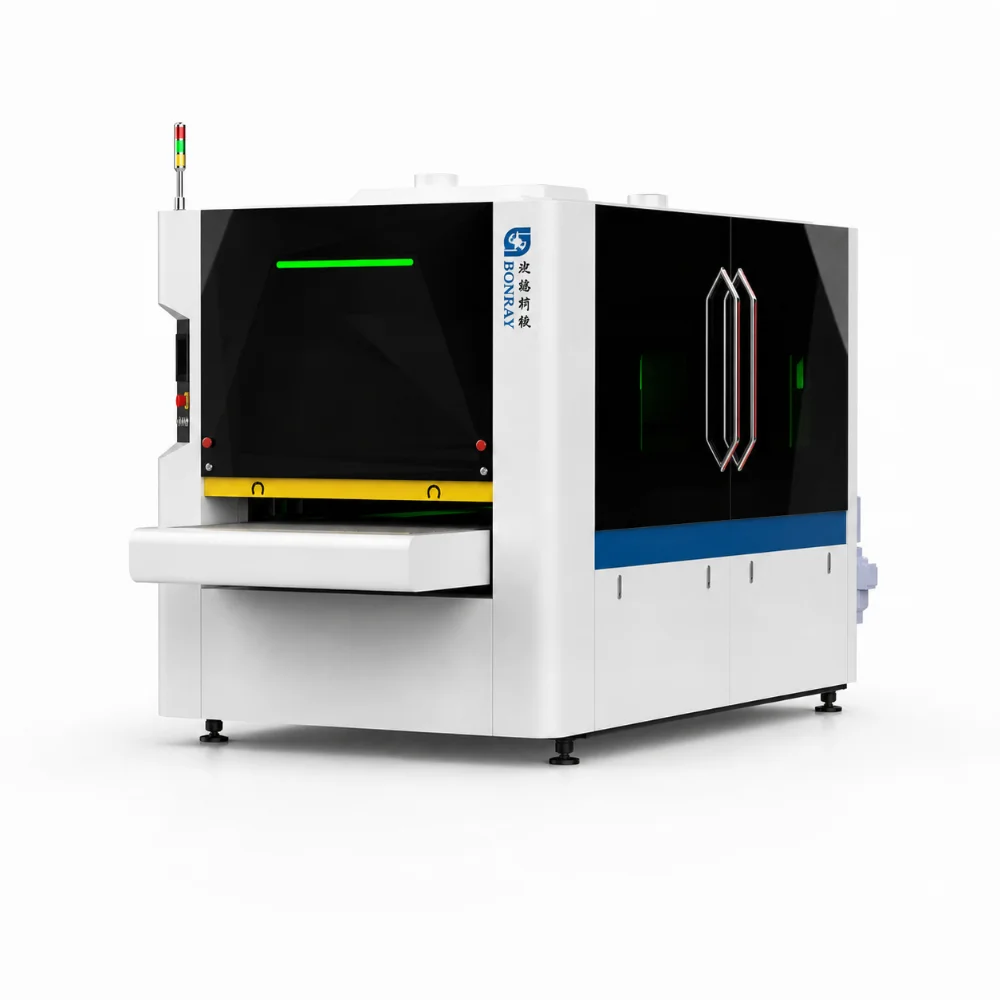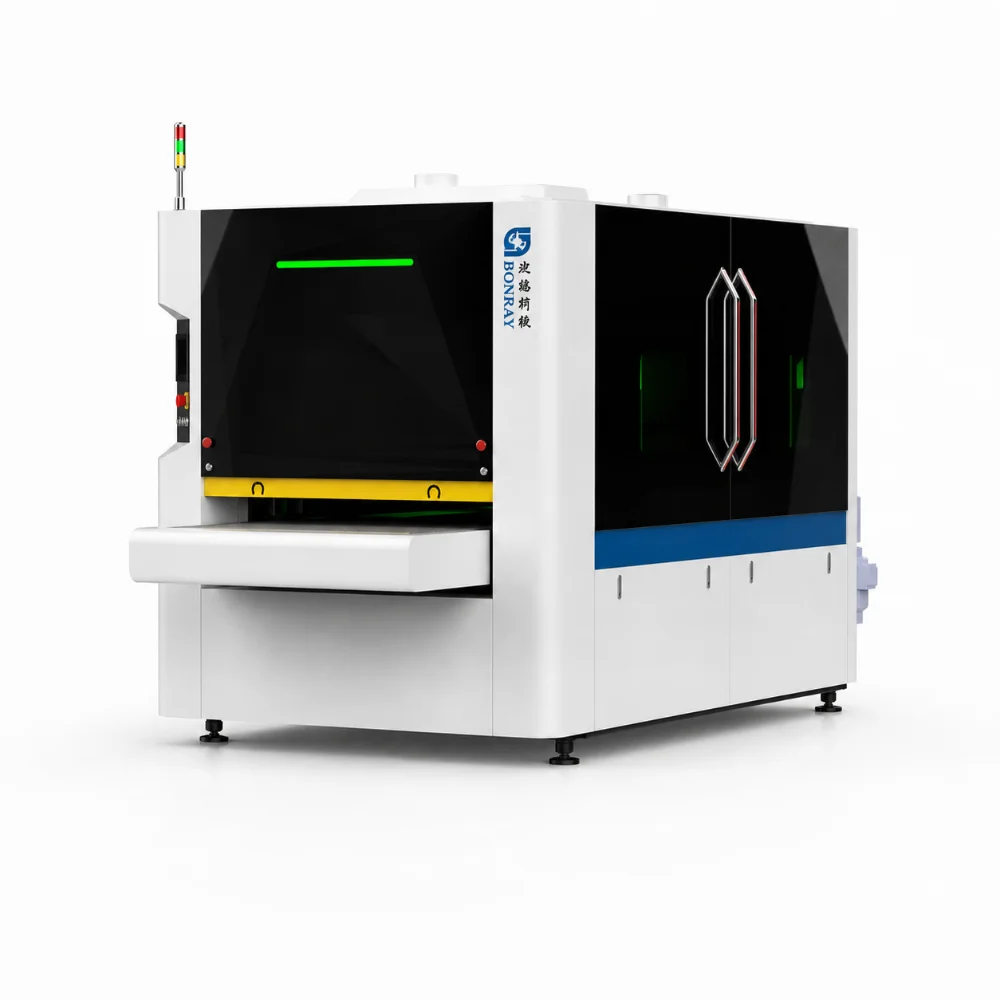
Deburring for Sheet Metal Fabrication
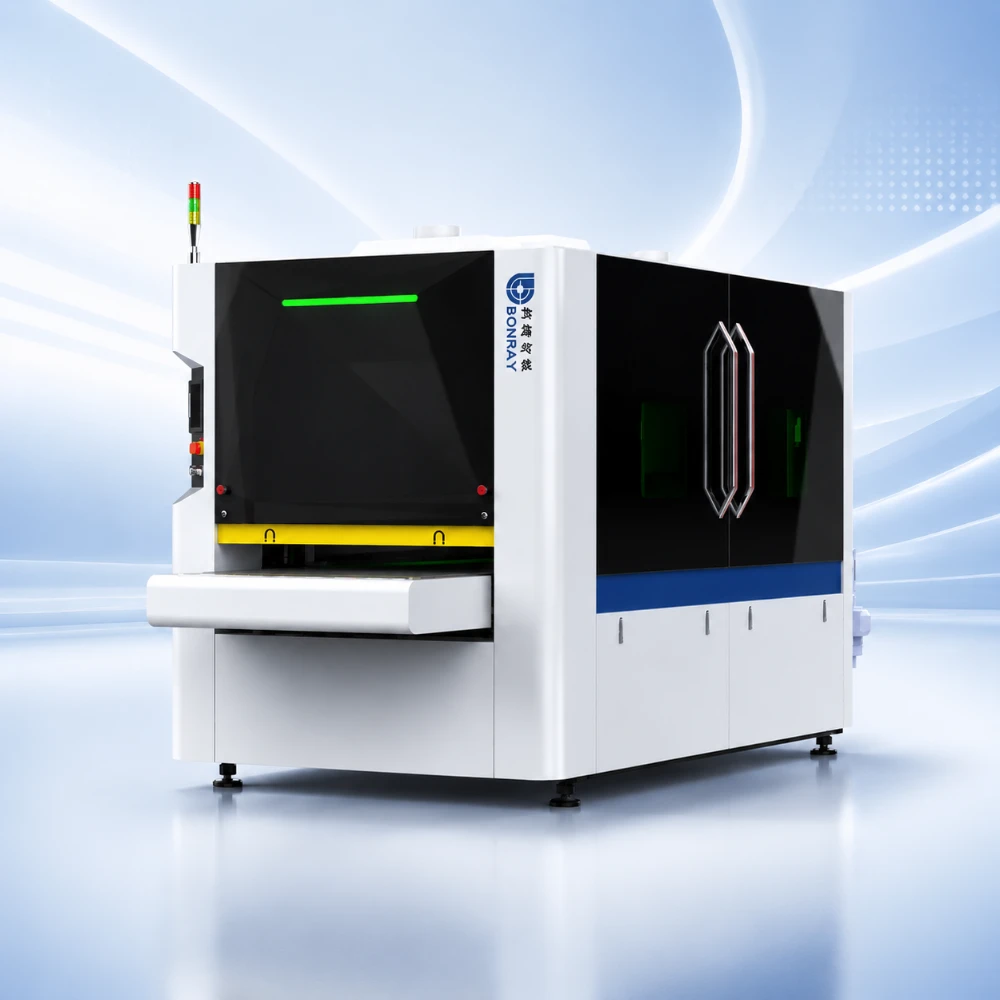
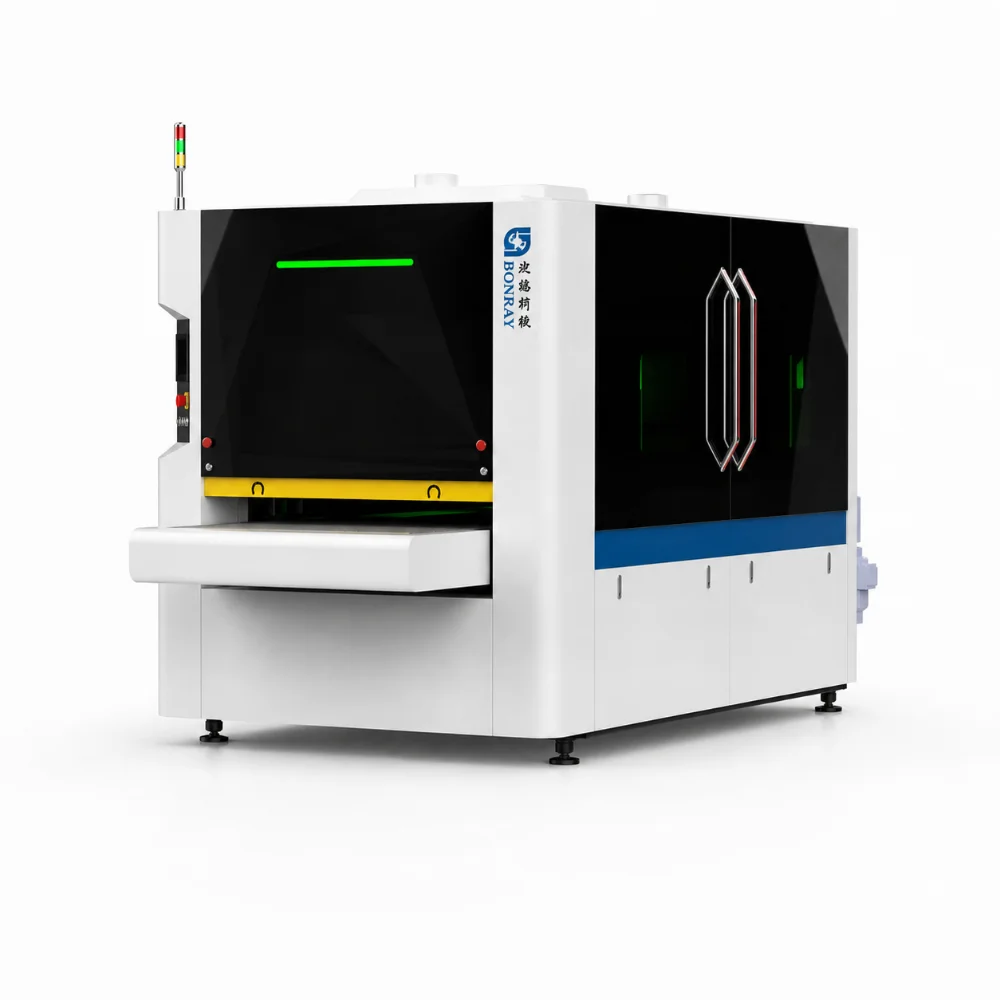
For laser-cutting subcontractors, enclosure manufacturers and sheet metal fabrication shops, burr removal is often the step between cutting and a part that can be handled, assembled or finished. This deburring process uses abrasive-belt stations to remove raised material from flat workpieces. A brush-equipped configuration can add contour treatment where the part also needs an edge break.
The practical starting point is the incoming part, not the name of the machine. A punched burr, a light laser-cut burr and strongly attached plasma dross can require different tooling and process sequences. Select the arrangement for the material that must be removed and the surfaces that must remain within tolerance.
Match the Stations to the Required Result
- Belt-only deburring: a BB-type arrangement removes raised material from the exposed face and performs initial surface grinding. It does not include an orbital brush stage for controlled contour rounding.
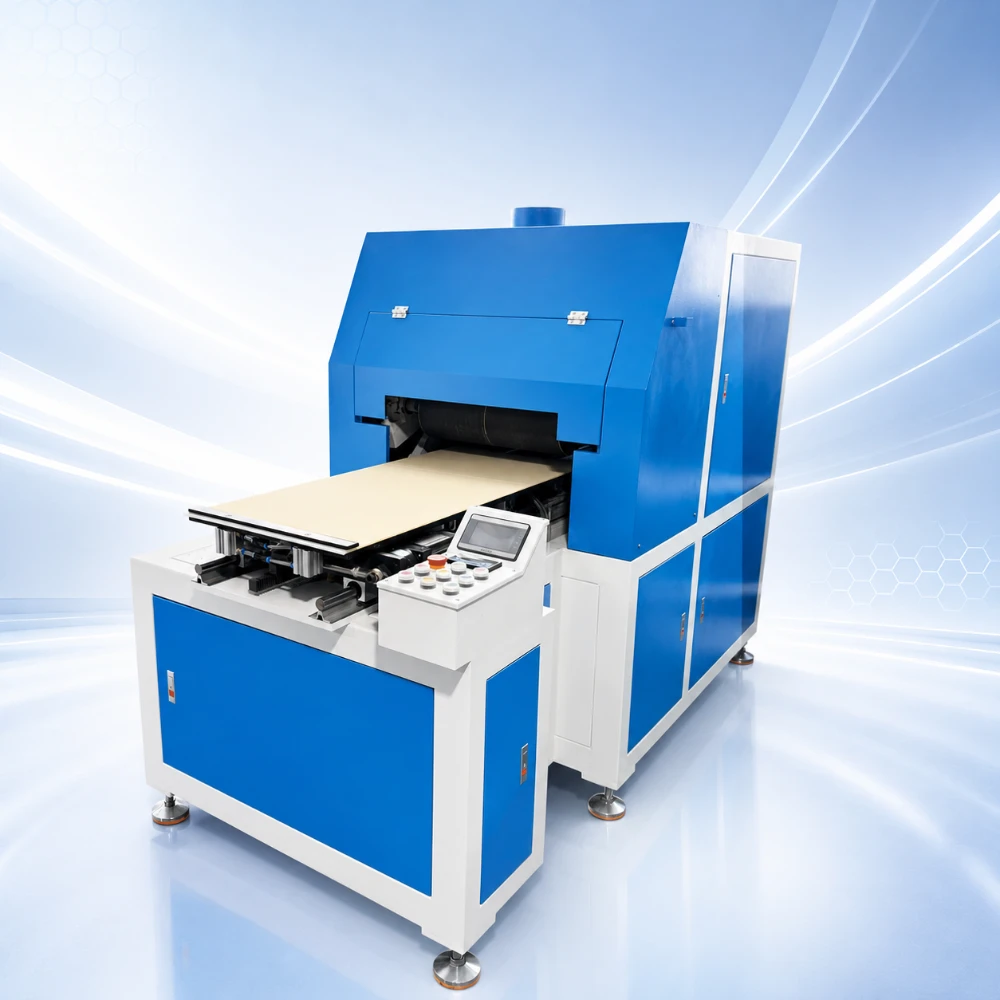
- Deburring with edge rounding: BBR and BRB arrangements combine abrasive belts and brushes. The order of those stages matters when the final face texture is also specified.
- Heavy attached dross: assess a hammer-stage arrangement before fine abrasive processing rather than treating heavy slag as an ordinary small burr.
How Wide-Belt Deburring Works
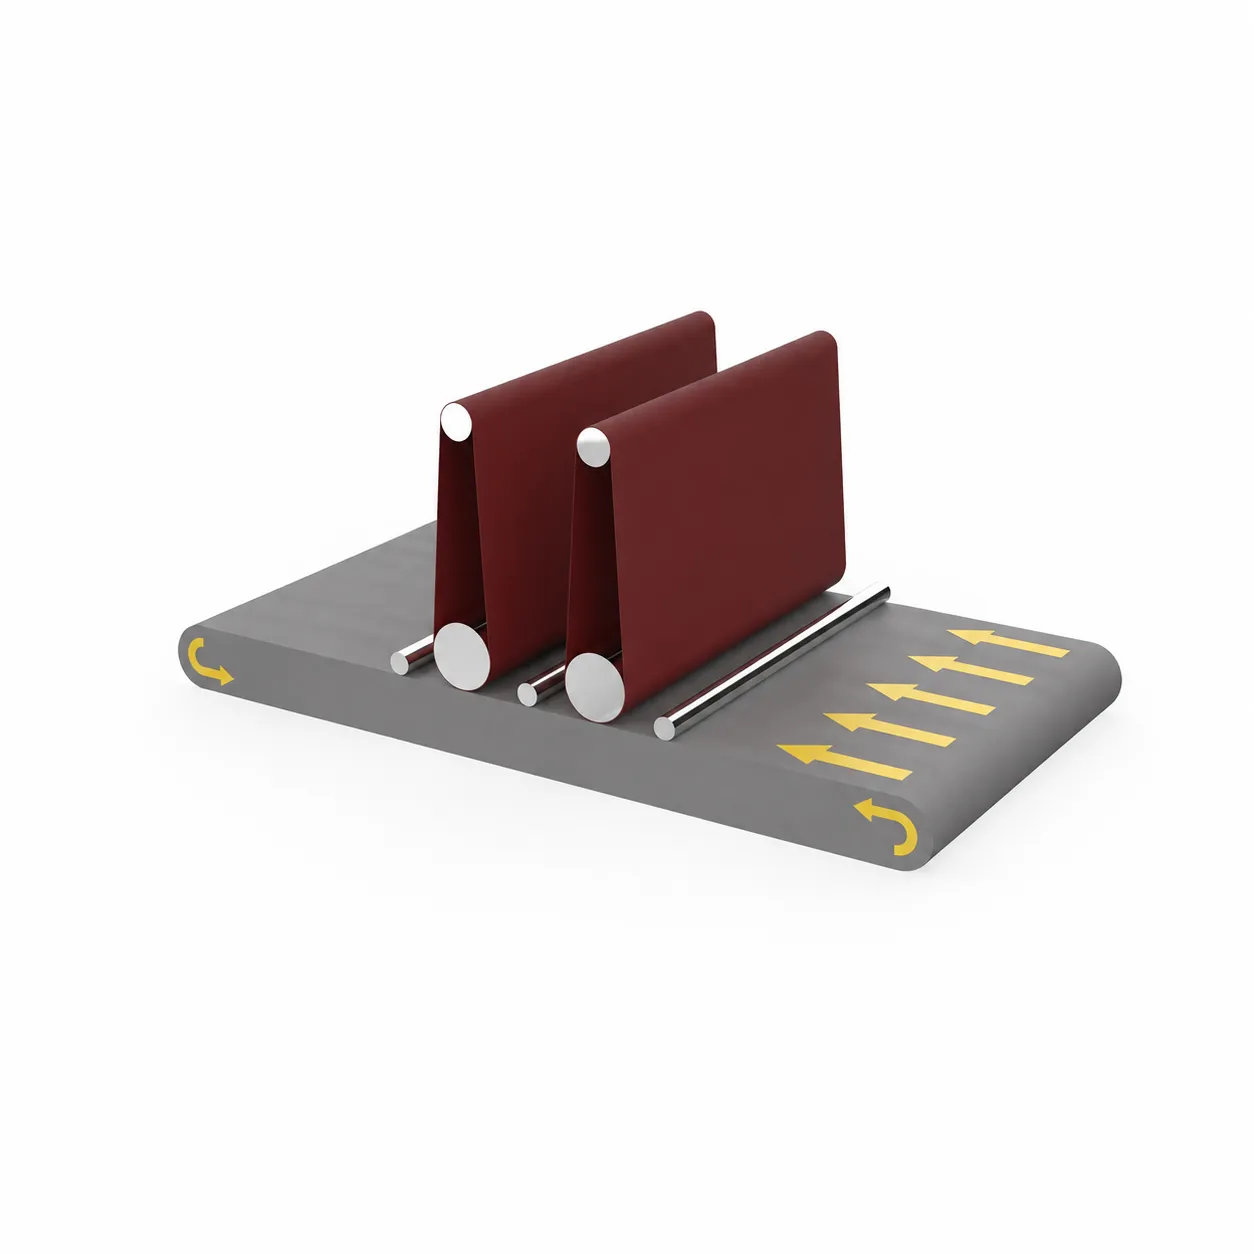
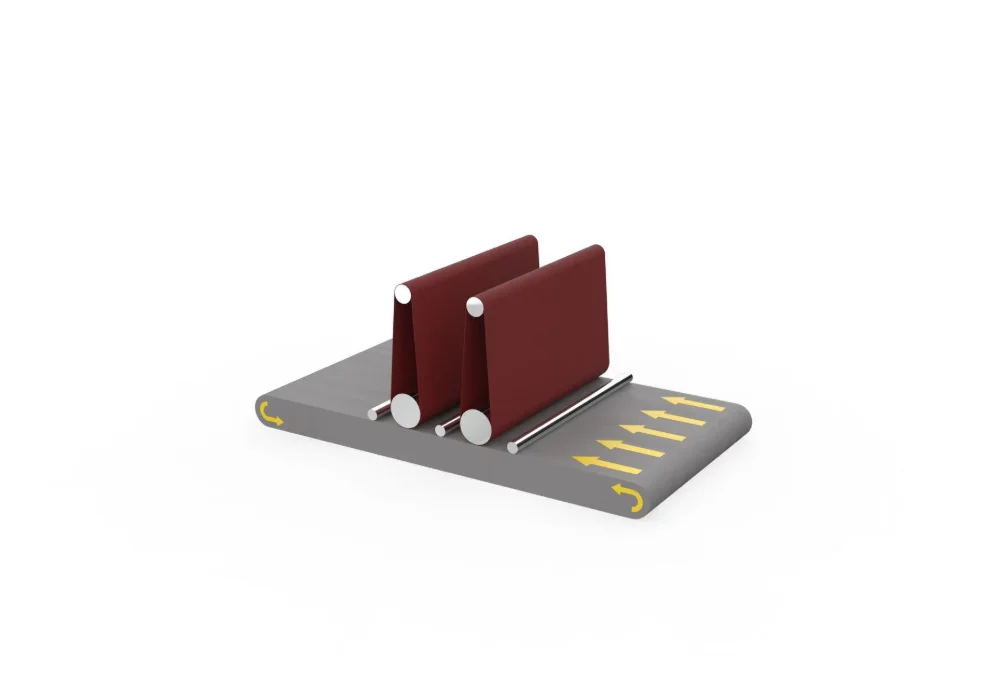
The workpiece travels on a conveyor beneath the abrasive stations. Machine-height settings establish contact with the exposed face; the belt grit, contact setting and feed speed are chosen together. Start with the amount and position of the burr, then check the stock-removal allowance on the drawing. A more aggressive setting can remove a burr but also change thickness, marks or dimensions.
The underside is not automatically processed by an upper-face conveyor arrangement. Identify whether one face or both faces need treatment and confirm the handling and pass sequence before evaluating output.
Where a Brush Stage Helps
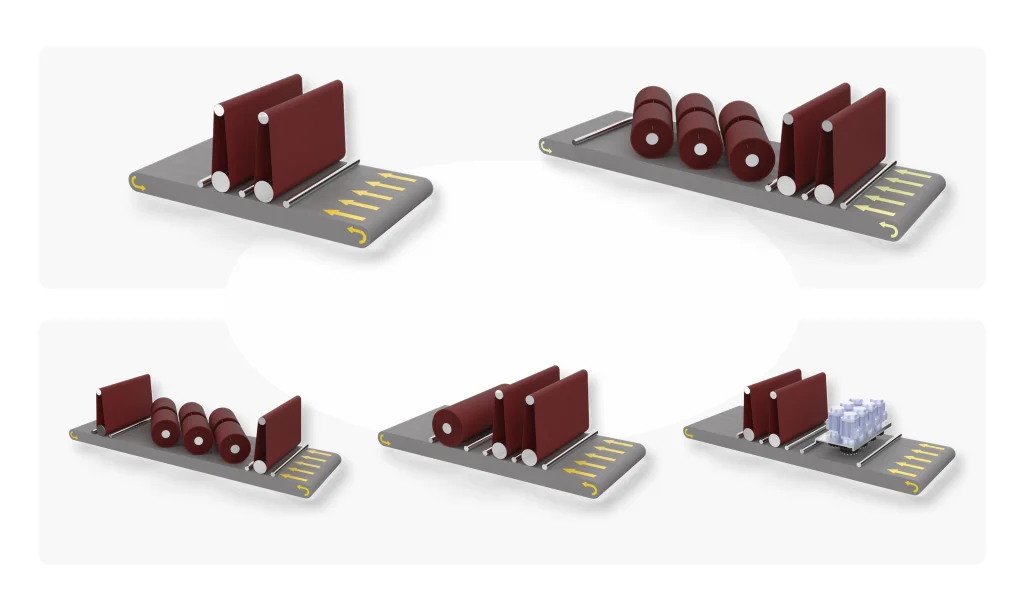
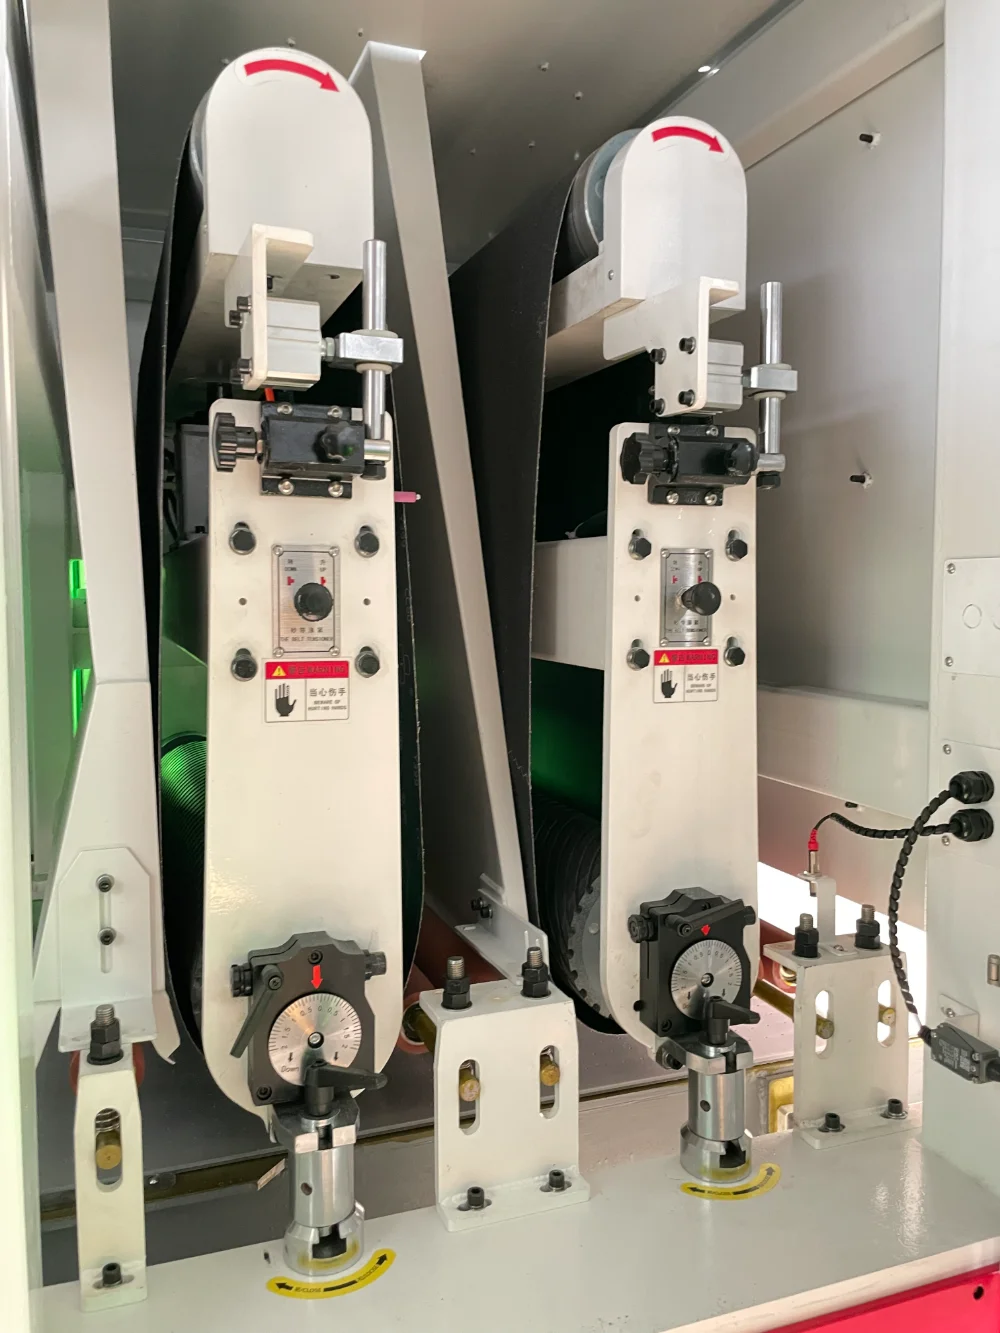
A brush stage treats accessible outer contours and hole edges after the main raised material has been removed. In the 1000BRB technical arrangement, two sanding-belt units are combined with six brush rollers in three staggered rows. That describes a particular station layout, not standard equipment on every deburring machine.
For perforated parts, small blanks and thin sheets, work holding is as important as the abrasive. Review the area supported by the conveyor, part flatness and open area around holes. Vacuum suction is configuration-dependent: the product catalogue lists it as an option, while the 1000BRB technical arrangement includes a suction platform and blower.
Workpiece Information for Selection
| Workpiece information | Why it matters |
|---|---|
| Material, thickness and part dimensions | Defines the suitable machine and hold-down arrangement. |
| Burr location, height and attachment | Determines whether belt grinding alone is sufficient. |
| Smallest part and hole geometry | Checks support and tool access. |
| Required edge condition and surface texture | Defines the abrasive sequence and acceptance sample. |
| Permitted stock removal and production volume | Sets trial conditions and evaluates throughput. |
Check the Trial Part and Production Setup
- Inspect the treated face and each specified contour for remaining burrs, excessive edge loss and unacceptable surface marks.
- Include the smallest and largest parts, the most difficult burrs and any highly perforated examples in the trial batch.
- Record the abrasive sequence, feed settings and inspection sample for repeat work; review the setup as abrasives wear or incoming material changes.
- Confirm the selected working width, thickness capacity, electrical supply, compressed air and dust-extraction scope. Working width alone does not establish minimum-part handling.
There is no single fixed capacity table for this application page. Confirm the exact BB, BBR or BRB model and supplied stations before using a catalogue specification for purchasing or installation.
Use slag removal for heavy cutting deposits, edge rounding for the specified contour profile and surface finishing for a controlled visible face texture.