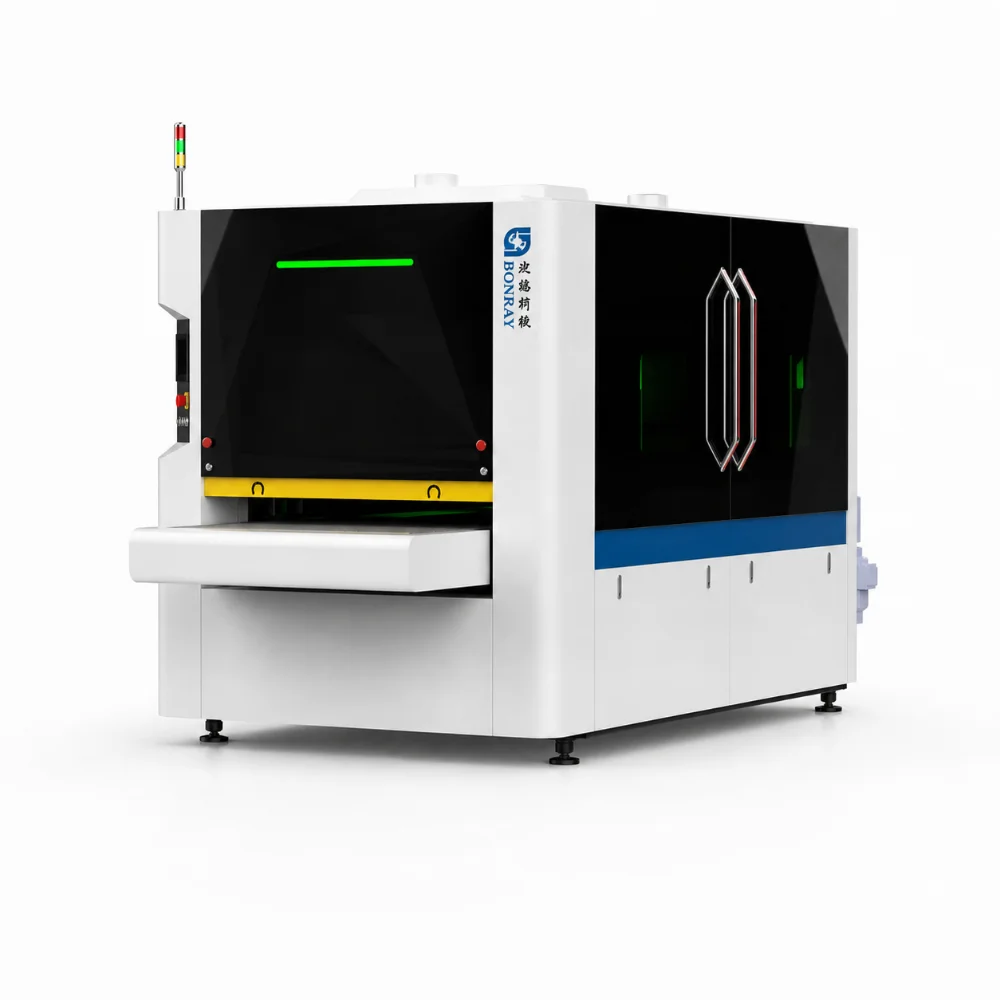
Surface Finishing for Visible Sheet Metal Components
Manufacturers of visible panels, equipment covers, enclosures and decorative fabricated parts need more than a generally clean surface: adjacent components must present the intended grain and appearance. Belt and roller finishing prepares the exposed face of stainless steel, brass and aluminum sheet parts against an approved sample.
Select this process when the requirement is a directional brushed, satin or matte appearance. Define the incoming surface, the final visual standard and the material-removal allowance before deciding the abrasive sequence. Finish names alone do not establish a measurable acceptance specification.
Choose the Grain and Surface Texture
- Directional grain: a belt stage establishes a visible scratch direction; agree its orientation relative to the finished part and adjacent panels.
- Satin or matte appearance: compatible non-woven abrasives and finishing rollers refine the face after initial preparation.
- Special textures: snowflake and other named decorative patterns require a specifically matched tool arrangement and sample approval; they are not supplied by every belt-and-roller setup.
Belt Preparation Followed by Finishing
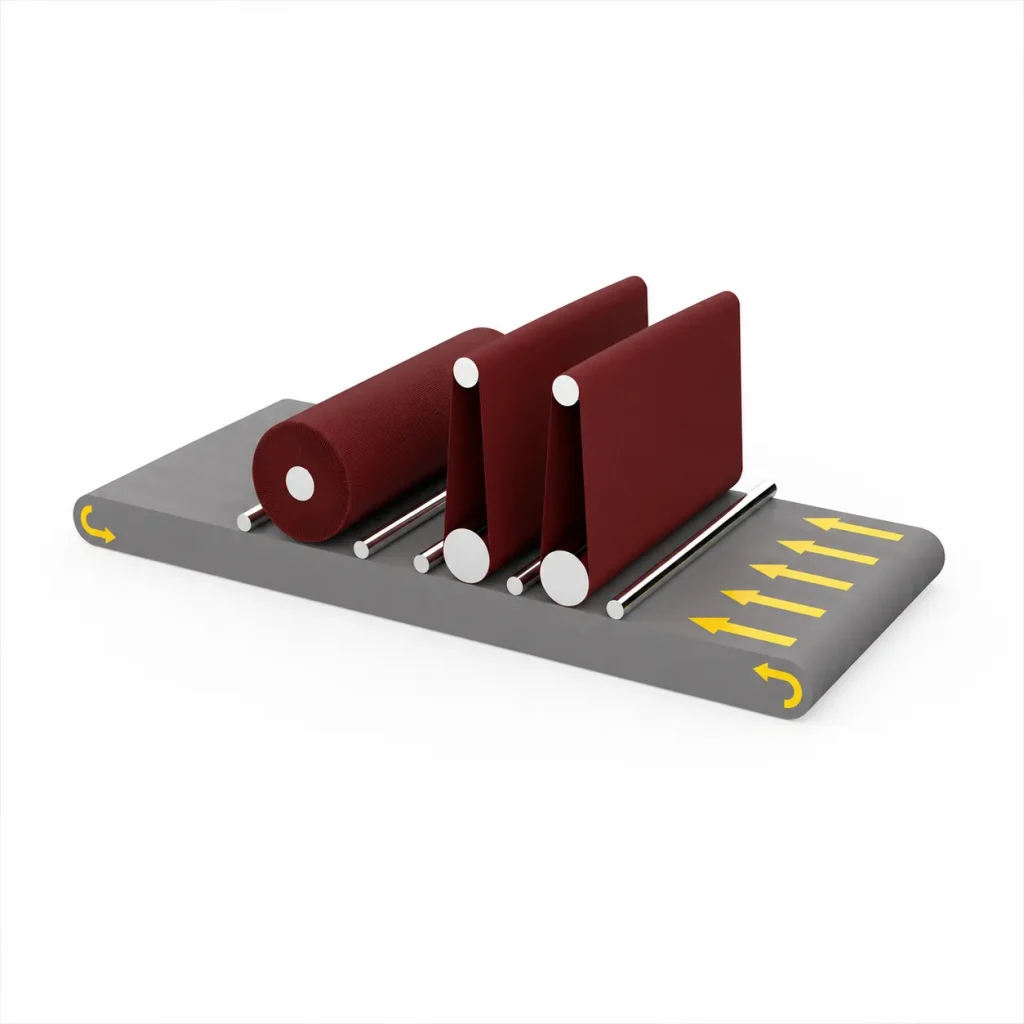
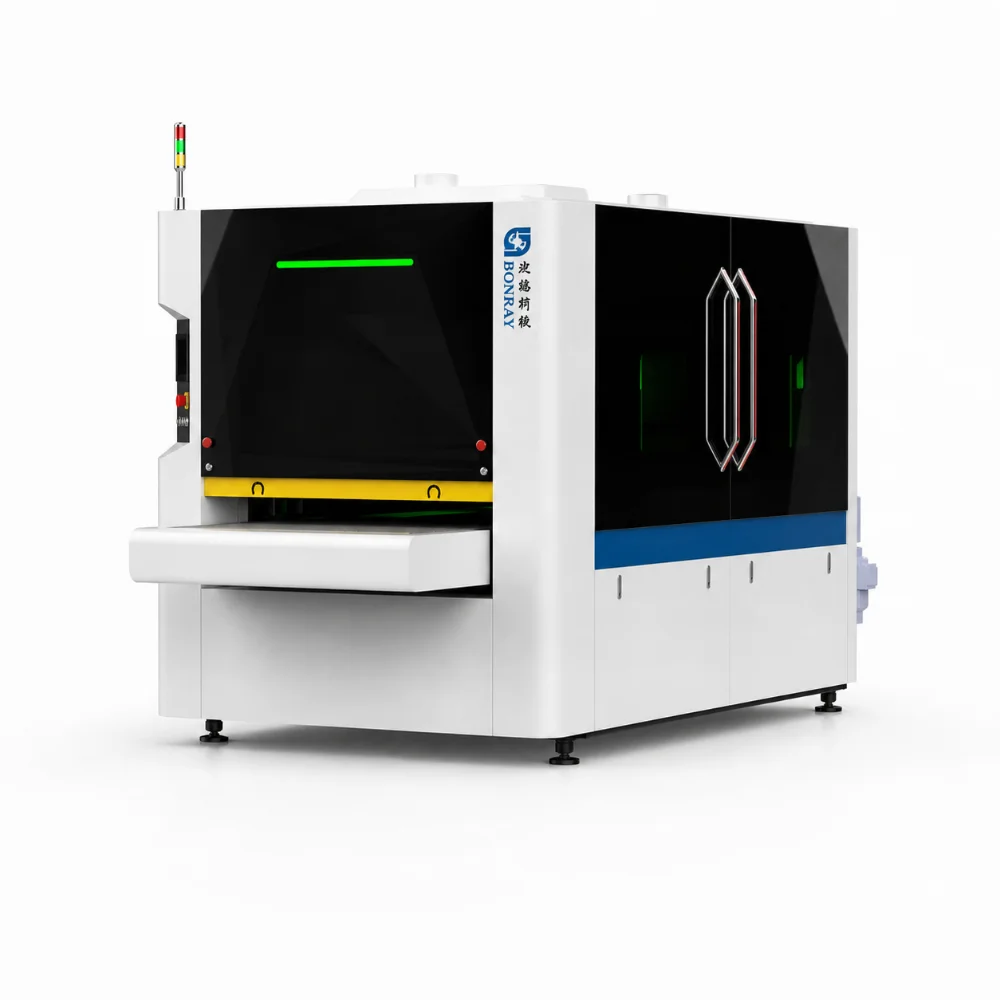
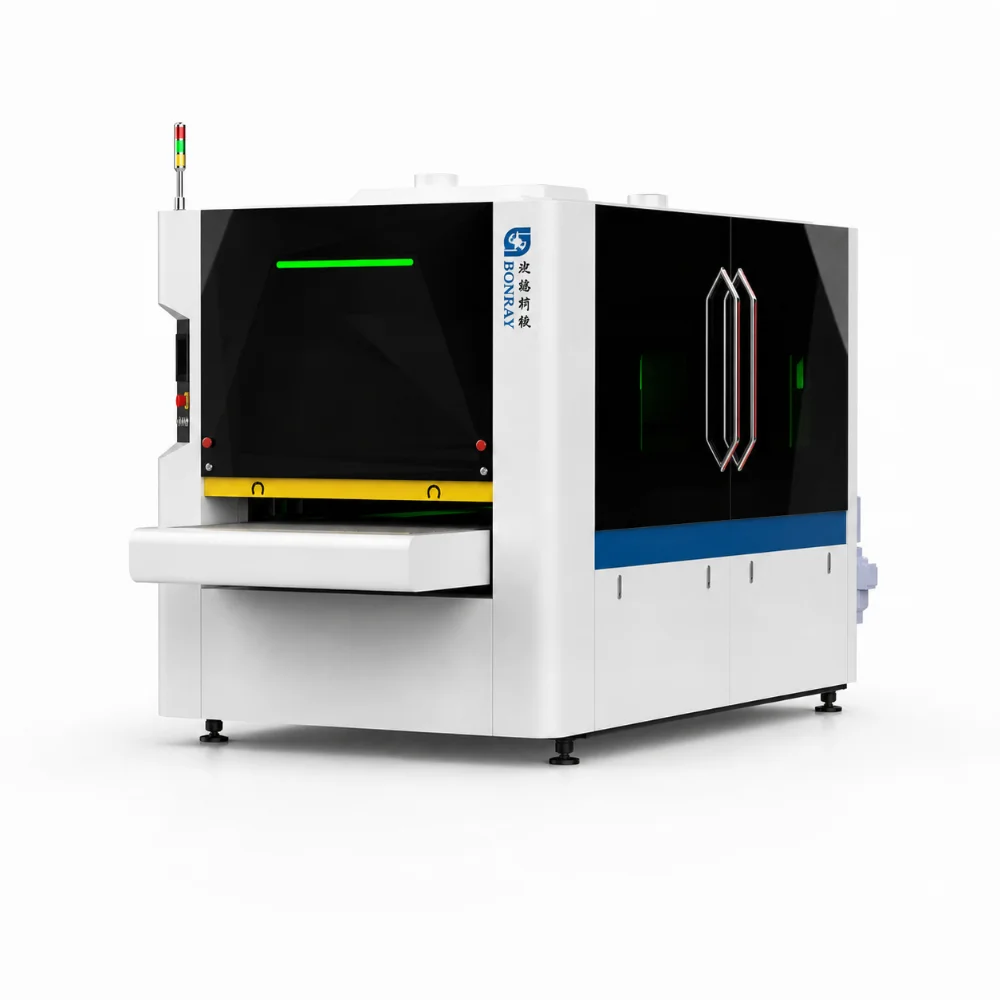
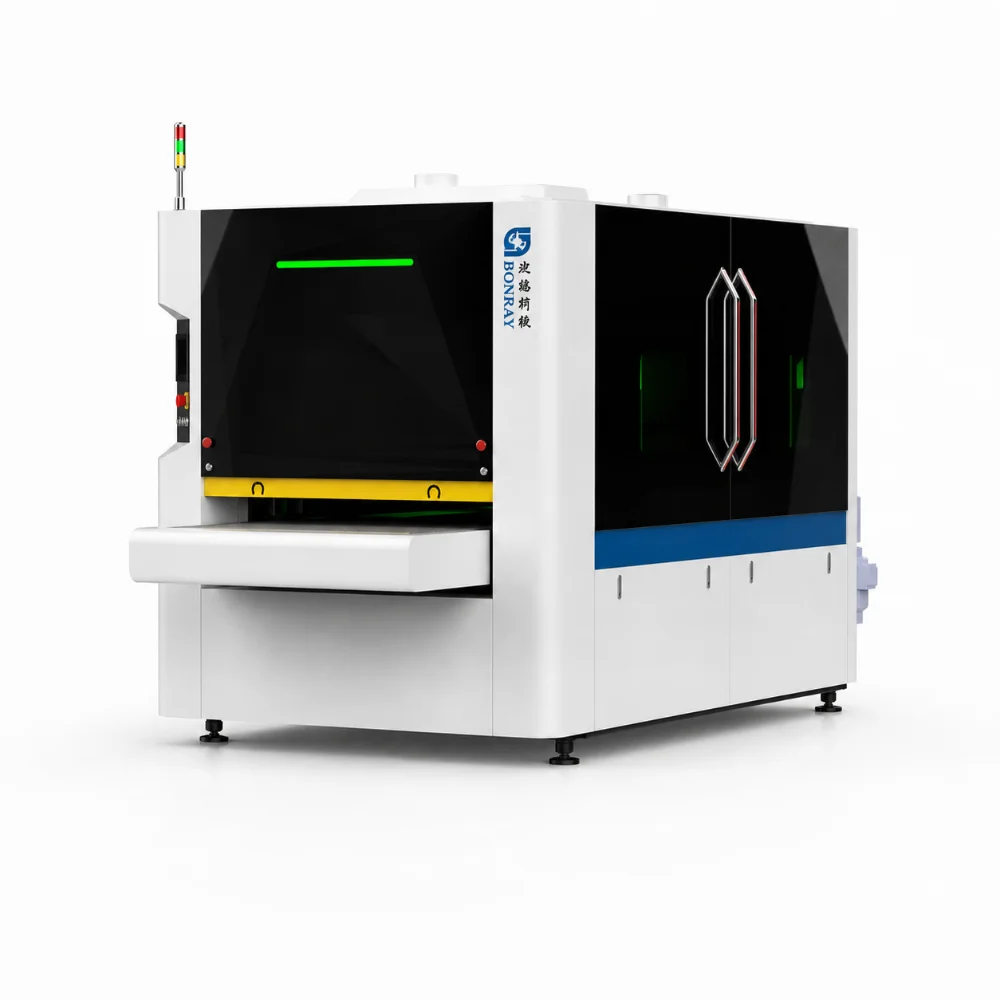
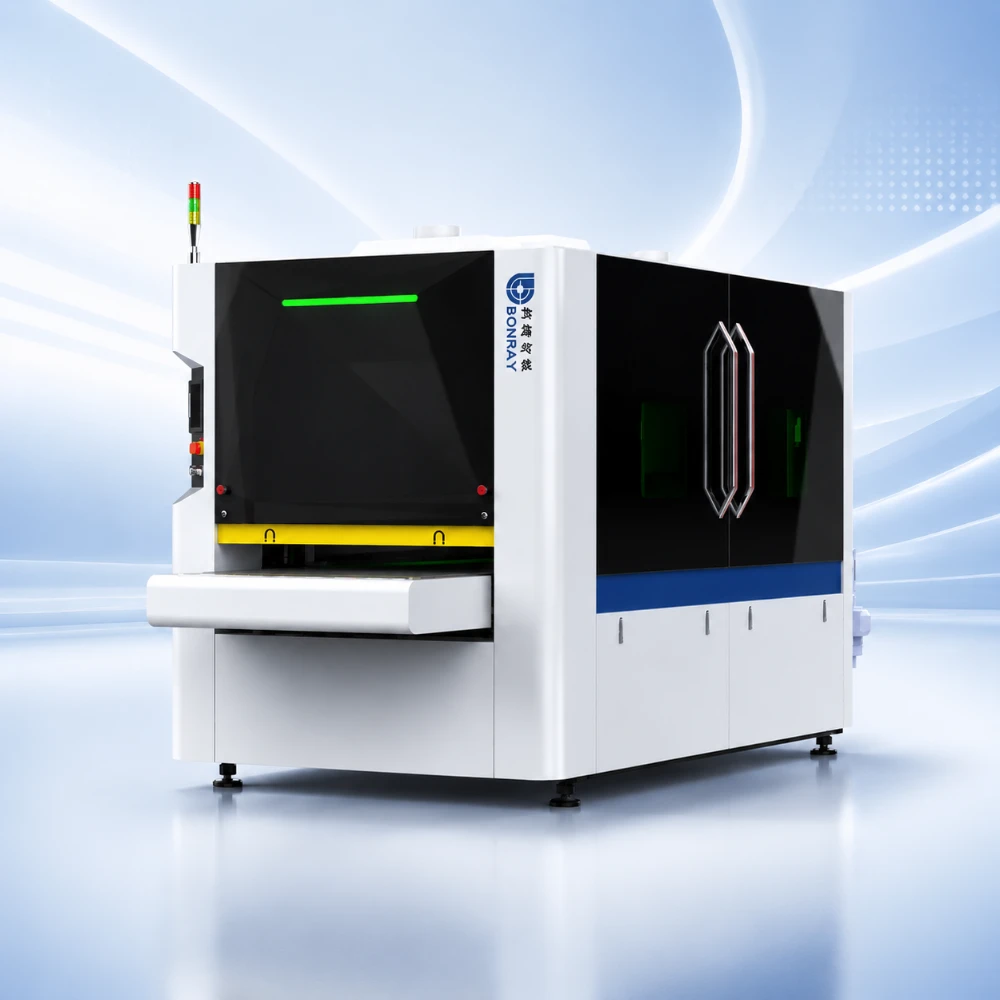
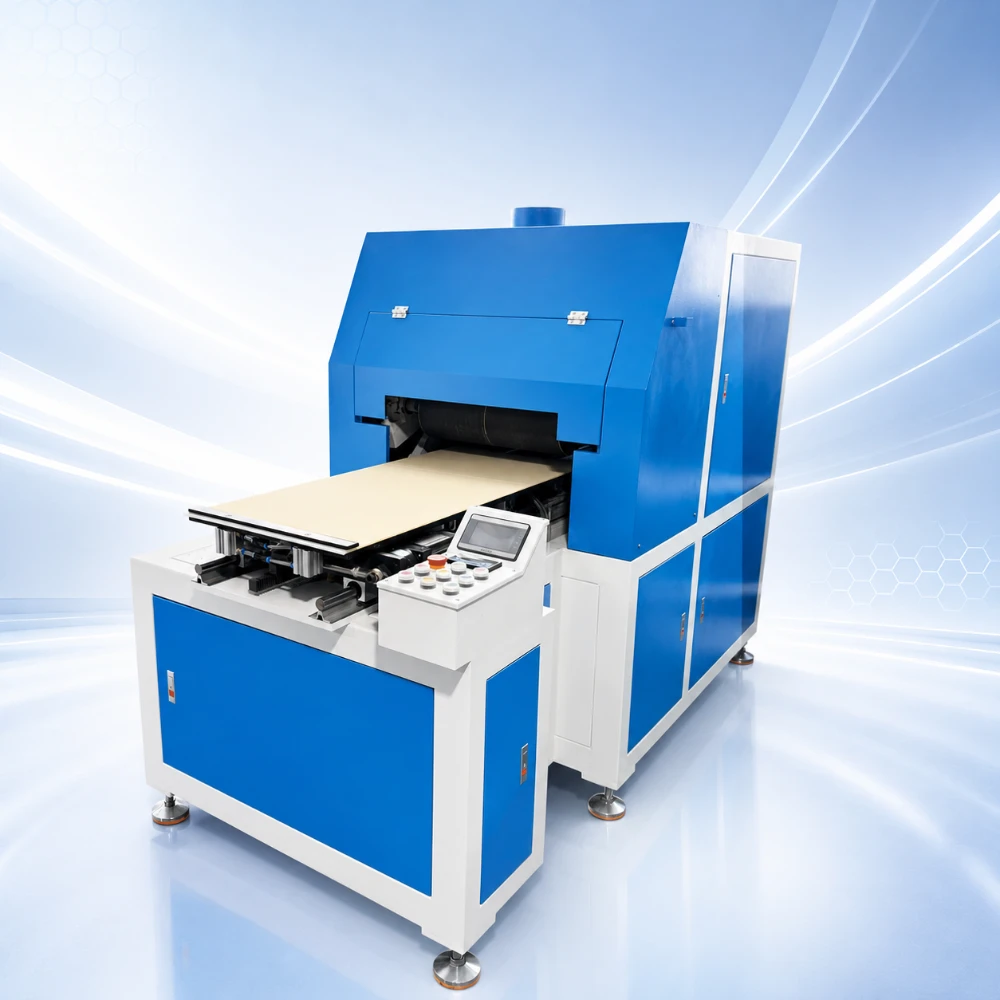
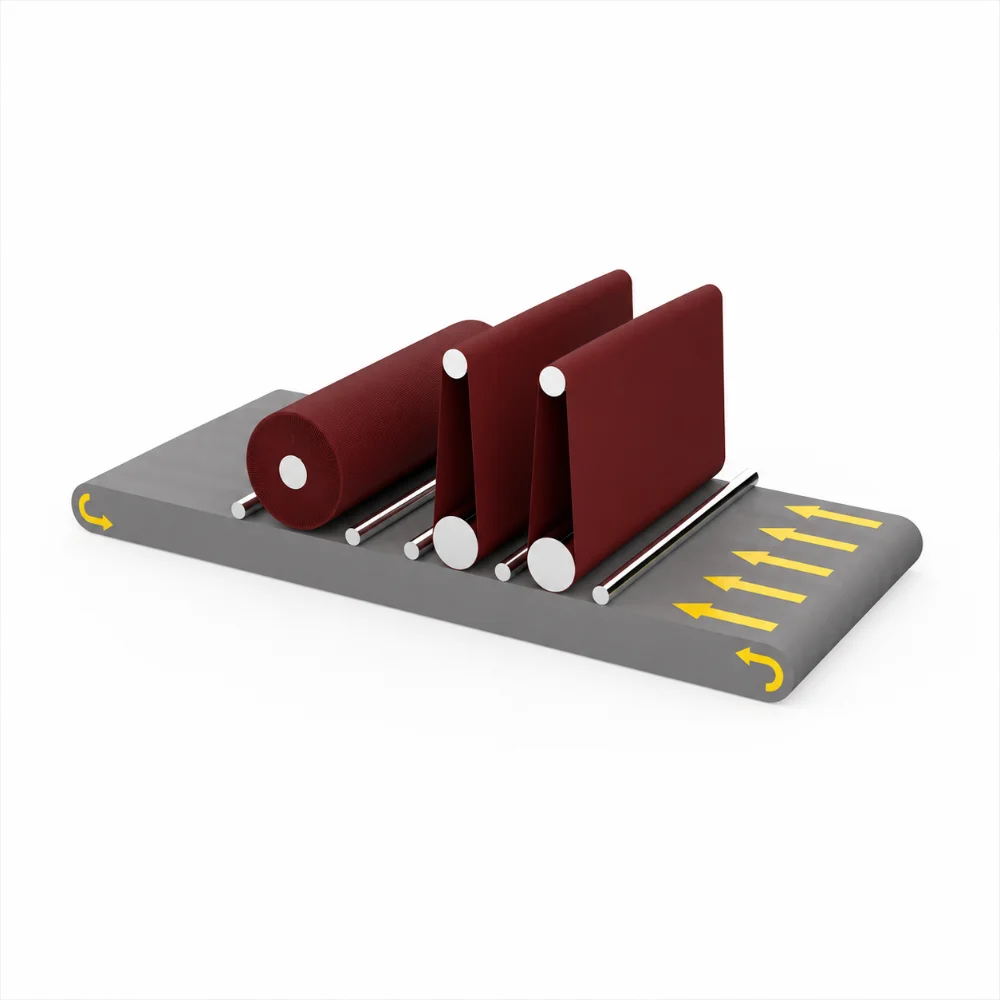
A conveyor carries the flat workpiece under the selected contact stages. Abrasive belts remove and blend material on the exposed face; the abrasive type, grit, contact setting and feed speed determine the scratch pattern and removal. A finishing roller can then refine the appearance. The BBW catalogue arrangement illustrates belt processing followed by a final finishing unit; a BRB arrangement places a belt after the brush stage for a different sequence.
Use the stations required by the actual part. Burr removal, contour rounding and decorative face finishing are separate tasks even when they share one enclosure. Neither a finish name nor an abrasive grit establishes that all three operations are included.
Non-Woven Roller Finishing
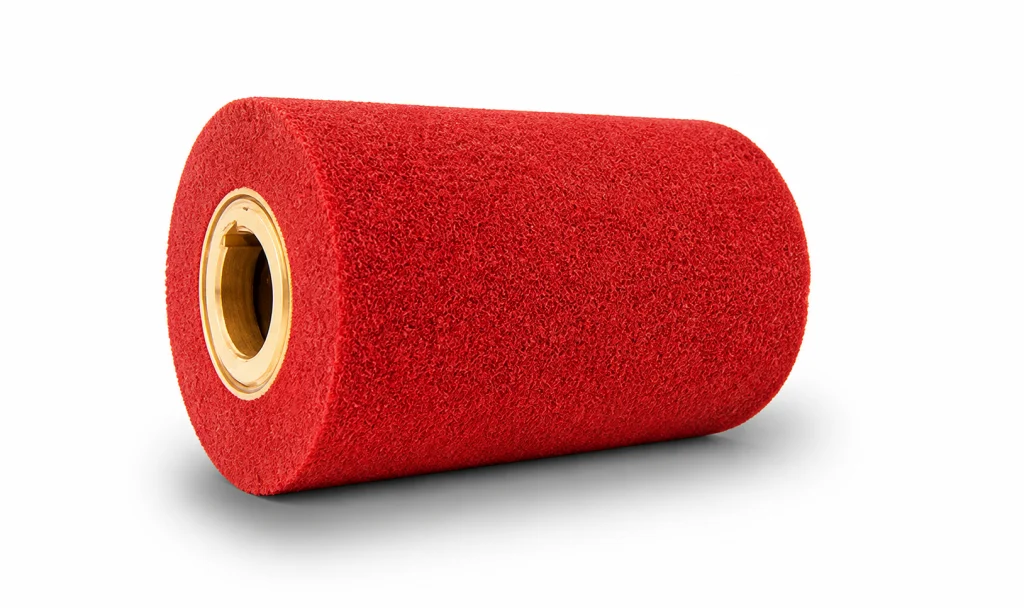
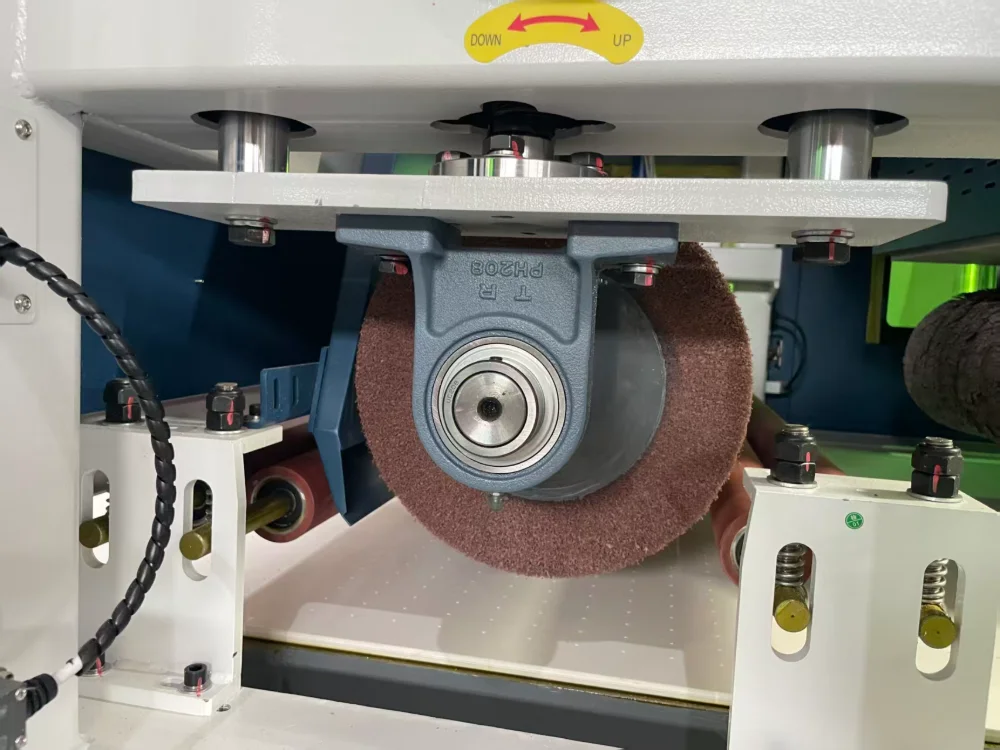
A non-woven abrasive roller blends the prepared surface through its selected abrasive grade and contact setting. This tooling example shows a finishing consumable, not a complete machine or proof of a particular measured roughness. Deep scratches and substantial defects must first be assessed against the permitted stock removal; a fine roller cannot be assumed to erase them.
Approve Appearance Before Repeat Production
- Provide a representative incoming part and an approved finished sample with the required grain orientation.
- Inspect the first finished part under the agreed lighting and viewing direction. Compare adjacent-panel appearance where the assembly makes differences visible.
- Where roughness matters, specify the numerical target and measurement method separately from the visual texture.
- Record the belt/roller grades and validated settings, then monitor marks and appearance as abrasives wear or material batches change.
Plan the Incoming-Part Preparation
| Incoming condition | Process consideration |
|---|---|
| Raised burrs or attached cutting residue | Complete primary removal before decorative finishing. |
| Existing scratches | Check depth against the permitted material removal. |
| A visible grain requirement | Agree direction, uniformity and the appearance sample. |
| Parts intended for coating | Match preparation to the specified pretreatment and coating system. |
| Mixed materials or changing batches | Review abrasive selection, cleaning and process settings. |
Machine Scope and Material Handling
Confirm working width, thickness range, smallest-part support and whether one face or both faces require treatment for the selected model. Vacuum handling and dust extraction must be specified for the actual arrangement; they cannot be inferred solely from a family illustration. Also agree how clean finished parts will be handled and protected before the next operation.
This application page does not provide a fixed machine-capacity or roughness guarantee. A brushed or satin appearance is not an 8K mirror finish, and surface finishing alone does not establish coating adhesion. Use the approved sample and downstream preparation requirements to judge the complete process.
Prepare raised burrs with deburring and sharp contours with edge rounding. For a distinct mirror-polishing requirement, see the flat metal mirror polishing machine.